شعار
وطن

غرفة اختبار الصدمة الحرارية

المحفوظات
العلامات

غرفة اختبار الصدمة الحرارية

  • Lab Companion Rapid Temperature Change Test Chamber: Wide Temperature Range & High Precision for Stringent Thermal Cycling Reliability Testing Lab Companion Rapid Temperature Change Test Chamber: Wide Temperature Range & High Precision for Stringent Thermal Cycling Reliability Testing
    Oct 22, 2026
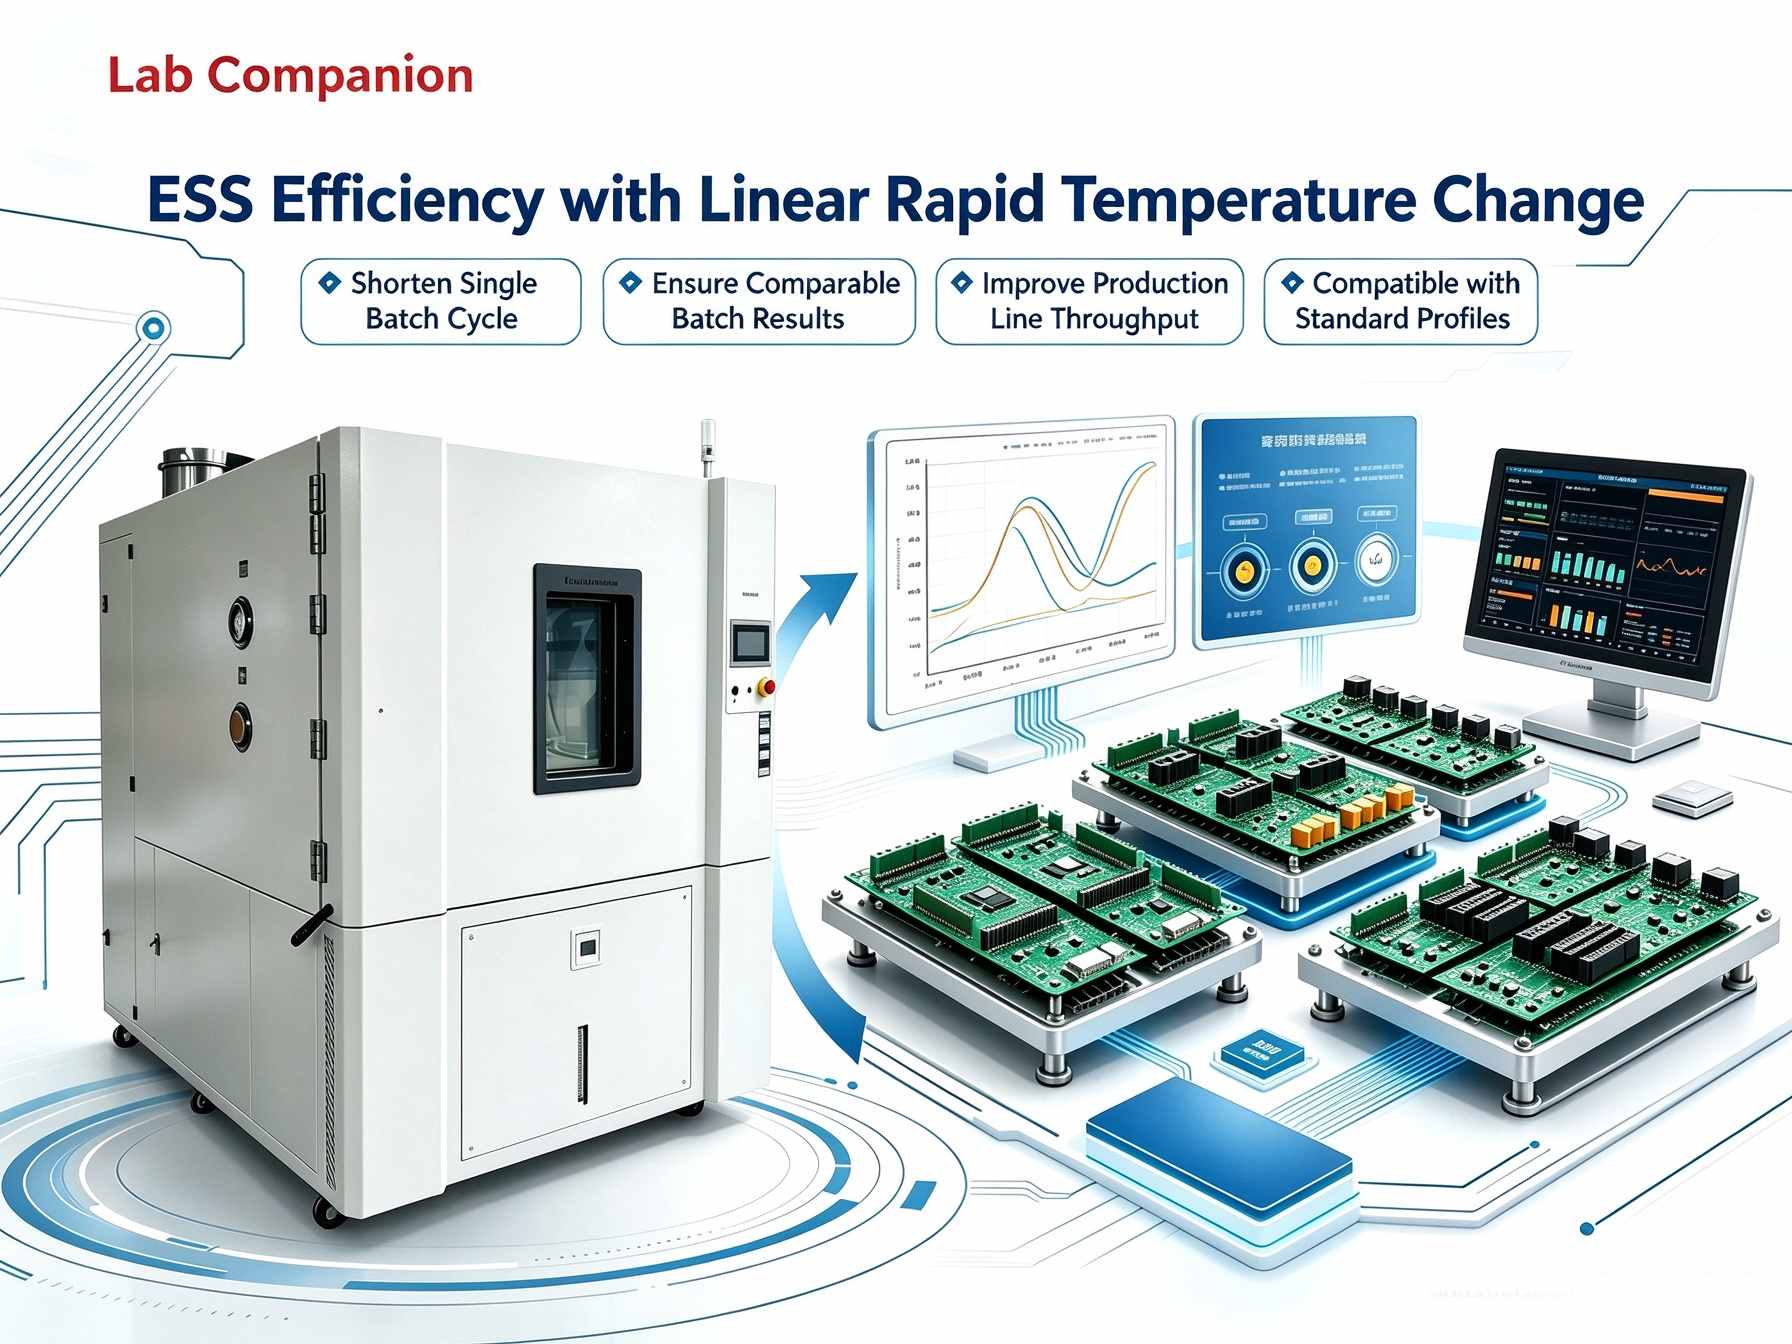
    Rapid Thermal Cycling: The Accelerator for Reliability Validation Reliability testing is no longer merely to verify whether a product “works”. Its core goal is to efficiently trigger and uncover latent defects. The rapid temperature change test chamber delivers controlled high temperature ramp rates to repeatedly apply thermal stress within a short cycle, cutting validation time and helping teams accelerate R&D iteration and production screening. As a national high-tech enterprise rooted in Dongguan, Lab Companion specializes in the R&D and manufacturing of environmental reliability test equipment. Serving the electronics manufacturing sector including semiconductors, automotive electronics and optical communications, our rapid temperature change chambers are engineered for demanding thermal cycling assessments. This article explains ramp rate specifications, failure acceleration mechanisms, key equipment features and selection guidelines. 1. Understanding Temperature Ramp Rate 1.1 What is Temperature Ramp Rate Temperature ramp rate refers to the speed of temperature rise or fall per unit time, measured in ℃/min. It is the core performance metric for rapid thermal cycling chambers. A higher ramp rate shortens each thermal cycle, allowing more cycles to be completed within the same test window and improving overall test throughput. 1.2 Multiple Ramp Rate Options Lab Companion rapid temperature change test chambers offer linear ramp rates of 5℃/min, 10℃/min and 15℃/min: 5℃/min: For standard thermal cycling qualification 10℃/min: Compliant with most industrial test specifications 15℃/min: Optimized for high-efficiency ESS (Environmental Stress Screening) 1.3 Controlled Linearity Matters More Than Raw Speed Faster does not always mean better. Non-linear temperature transitions easily lead to temperature overshoot and internal condensation, introducing artificial stress that may damage precision components and invalidate test results. A reliable rapid thermal cycling chamber must deliver both fast response and stable, linear temperature control. 2. How Rapid Thermal Cycling Accelerates Failure Detection 2.1 Thermal-Mechanical Stress to Expose Hidden Defects Electronic assemblies consist of multiple materials with different coefficients of thermal expansion (CTE). During rapid temperature swings, mismatched expansion and contraction generate concentrated thermal-mechanical stress at material interfaces. Higher ramp rates amplify this stress, revealing latent failures such as solder fatigue, package cracking and interface delamination at an earlier stage. 2.2 Shorter R&D Cycles for Faster Design Iteration Engineers often evaluate multiple design variants within tight schedules. High ramp rates reduce cycle duration, enabling the required number of thermal cycles to finish sooner. This speeds up design comparison, optimization and new product launch. 2.3 Efficient Production Screening for Quality Control In mass production screening, rapid thermal cycling cuts per-unit test time and increases factory throughput. The intensified thermal stress effectively weed out early failure units from batches, balancing screening effectiveness and production tact time. 3. Core Capabilities of Lab Companion Rapid Temperature Change Test Chamber 3.1 Wide Temperature Range with Margin for Severe Testing Standard models cover -70℃ to +150℃, covering mainstream thermal cycling requirements for semiconductors, automotive electronics and optical communications, with extra margin available for highly accelerated stress tests. 3.2 Multiple Linear Ramp Rates for Diverse Test Standards Selectable linear rates of 5 / 10 / 15℃/min support compliance with industry standards or internal stress screening, reconciling test validity and productivity. 3.3 High-Precision Temperature Control for Reproducible Results Temperature fluctuation ≤ ±0.3℃; temperature deviation ≤ ±2℃. Stable thermal field performance is maintained even under fast ramp conditions, ensuring comparable and repeatable test data across different batches and shifts. 3.4 Batch Testing & Data Traceability for Digital Quality Management Multi-layer racks support simultaneous testing of multiple samples to boost capacity. The system automatically logs temperature profiles and test records, satisfying digital quality control and traceability requirements. 4. Selection Guide for Rapid Temperature Change Test Chambers 4.1 Define Ramp Rate Based on Test Specifications First confirm the mandatory ramp rate stated in your test standard. For internal screening without fixed standards, higher ramp rates can be considered, with special attention to linear control performance. 4.2 Match Temperature Range and Accuracy Requirements The chamber working range must fully cover your test limits with sufficient margin. Precision specifications should guarantee consistent judgement. Lab Companion’s -70℃ ~ +150℃ range and tight control accuracy fit most common application scenarios. 4.3 Balance Throughput and Sample Protection While high ramp rates improve efficiency, excessive thermal stress may cause unintended damage to DUTs (devices under test). Select ramp rates and loading configurations according to material and structural characteristics. Custom solutions are available upon request. 4.4 Prioritize Long-Term Stability and Technical Support Rapid thermal cycling tests often run continuously for extended periods. Equipment reliability and vendor support directly affect R&D and production schedules. Choose a manufacturer with mature production capability and a comprehensive service network to secure stable operation over the full equipment lifecycle. Conclusion A rapid temperature change test chamber is a powerful tool that turns controlled thermal stress into actionable reliability insights. Equipped with wide temperature coverage, adjustable linear ramp rates, high-precision control, batch testing and data traceability, Lab Companion rapid thermal cycling chambers help R&D and QA teams expose product weaknesses faster and streamline validation workflows. Moving forward, Lab Companion will keep focusing on environmental reliability testing, delivering robust equipment and professional service to help industries uphold strict quality standards.
    إقرأ المزيد
  • Lab Companion Custom Thermal Cycling Chamber: Customization Path for Temperature Range, Internal Volume & Dimensions, Temperature Ramp Rate and Special Functions
    Oct 16, 2026
    I. Necessity of Non-Standard Customization 1.1 Performance Limits of Standard Models Thermal cycling chambers serve as core equipment for reliability testing in electronics, semiconductors, automotive electronics, new energy and other industries. Lab Companion TC series standard thermal cycling chambers feature a standard temperature range of -70℃ to +150℃, with 5 selectable temperature ramp rates from 5℃/min to 25℃/min. Available internal volumes range from 34L up to 16,000L. Popular standard sizes including 80L, 150L, 225L, 408L and 800L are kept in stock. These configurations meet most conventional thermal cycling test requirements. Nevertheless, standard models have inherent performance boundaries. They cannot directly support test tasks when test specimens exceed the inner chamber size, when required test temperature limits go beyond the standard range, when samples need power-on operation or connection to data acquisition systems, or when tests involve flammable and explosive specimens requiring special protection. 1.2 Practical Scenarios for Non-Standard Customization Non-standard customization is not an optional add-on, but a prerequisite to valid testing execution. Typical application scenarios are listed below: New energy vehicle battery pack testing: full battery packs require testing covering -40℃ cold start and 85℃ high-temperature cycling; Semiconductor chip testing: demand for infinitely adjustable ramp rates from 1℃/min to 20℃/min to match different phases of chip testing; High heat-load testing: operating samples may generate heat up to tens of kilowatts. Standard chambers lack sufficient cooling capacity to maintain specified ramp rates under loaded conditions. Founded in 2005 and headquartered in Dongguan, Guangdong, Lab Companion is a National High-Tech Enterprise and Guangdong Provincial Specialized & Sophisticated Enterprise. With over 20 years of expertise in environmental reliability test equipment, we operate three R&D and manufacturing bases in Dongguan, Kunshan and Chongqing. We have established a full-cycle customization system covering requirement evaluation, design, production and delivery. II. Four Core Customization Dimensions for Lab Companion Thermal Cycling Chambers 2.1 Temperature Range Customization The baseline temperature range of standard TC chambers is -70℃ ~ +150℃. For aerospace and other special test applications, the low limit can be extended down to -100℃, while the upper temperature limit can reach +250℃. We have delivered proven custom units with a precise range of -78℃ ~ +150℃ to comply with GJB 150.5A military environmental test specifications. For combined temperature & humidity testing, integrated solutions covering 20%RH ~ 98%RH are available. 2.2 Internal Volume & Dimension Customization Chamber size is the most frequently requested custom item. Custom volumes from 80L to 8,000L can be engineered as requested. Our walk-in chambers start at 1,000L up to 10,000L, with further scaling available upon request. Inner chamber design takes full account of specimen outer dimensions, loading arrangement (single / multiple samples), material access methods (handcart, forklift, hoisting) and requirements for powered sample testing. Lab Companion once delivered a 20m³ extra-large custom chamber for an aerospace research institute to solve reliability testing challenges for large aerospace assemblies. Note: Standard models of 80L, 150L, 225L, 408L and 800L are in stock. 2.3 Temperature Ramp Rate Customization Standard chambers offer 5 fixed ramp rates: 5, 10, 15, 20 and 25℃/min. Customised ramp profiles can be developed per test specifications. For semiconductor projects, we have realised infinitely adjustable ramp rates from 1℃/min to 20℃/min to accommodate varied heating/cooling requirements across chip test phases. 2.4 Special Function Customization Optional dedicated functions can be integrated according to test workflows: Semiconductor applications: Nitrogen purge to prevent condensation on samples at low temperatures; High heat-load applications: dedicated thermal load matching solution to stabilise ramp rates under loaded conditions; Control & communication: RS485 and Ethernet as standard; optional OPC UA and Modbus TCP for MES connection. For semiconductor production lines, SECS/GEM protocol can be customised to enable seamless data exchange between test chambers and factory management systems; Additional options: remote monitoring, probe station interfaces and integrated data acquisition systems. III. Delivery Workflow from Requirement to Commissioning 3.1 In-depth Requirement Analysis & Technical Alignment The project starts with multiple rounds of technical discussion. Our engineers identify not only what needs testing, but also test purposes and acceptance targets. Combining test standards, specimen characteristics, test cycles and on-site factory conditions, we translate customer requirements into quantifiable technical specifications. 3.2 Concept Design & Proposal Confirmation Preliminary equipment design is generated based on requirement analysis. Core parameters to be finalised include temperature range, ramp rate profile, inner chamber dimensions, structural layout, fixture & electrical interfaces and control system functions. The proposal will undergo technical review and confirmation with customers to ensure equipment specifications fully match test demands. 3.3 Manufacturing & Factory Acceptance Testing Once the proposal is approved, production commences. Our three manufacturing bases achieve an annual capacity of more than 2,000 units. Standard models are delivered within 7–15 working days, while non-standard custom chambers can be finished within 20 working days. Before shipment, both no-load and loaded performance verifications are completed. 3.4 On-site Acceptance & Operational Training After equipment arrival, we perform installation, commissioning and on-site acceptance. Acceptance items cover temperature range and ramp rate under no-load conditions, ramp stability under loaded conditions, temperature uniformity & fluctuation, program cycle validation, communication and data acquisition verification. We also provide on-site operation training and maintenance support to secure long-term stable operation. IV. Manufacturing & Service Capabilities for Custom Thermal Cycling Chambers 4.1 Production Capacity at Dongguan Manufacturing Base The Dongguan headquarters serves as our R&D centre and primary production site for TC series chambers, with a plant area of 27,286 m² and an annual output of around 1,000 environmental test chambers. Products hold EU CE certification. Supported by the complete supply chain in the Greater Bay Area, R&D, component procurement, assembly and factory calibration are completed locally to shorten lead times. 4.2 Nationwide Service Network Sales and after-sales service centres are located in Beijing, Shanghai, Wuhan, Chengdu, Chongqing, Xi’an and Hong Kong, forming a nationwide service network with fast response for customers in the Pearl River Delta. The company operates under ISO9001, ISO14001, ISO45001 and ISO27001 management systems. The Lab Companion trademark is registered under the Madrid System, with trademark protection across 27 EU member states, UK, Canada and multiple Southeast Asian countries. 4.3 Core Hardware & Control System TC series chambers adopt cascade refrigeration with compressors from top international brands. Lab Companion’s proprietary cold balance energy-saving control technology eliminates energy waste caused by conventional simultaneous heating and cooling conflict. The controller is our self-developed C100 PID + fuzzy logic temperature & humidity control system, equipped with a colour touchscreen. It supports multi-segment programming, automatic data logging, report generation, network connection, remote monitoring and cluster management. V. Selection & Acceptance Guidelines for Non-Standard Custom Chambers 5.1 Technical Agreement Confirmation The technical agreement is the primary acceptance document for custom equipment. It must clearly define: temperature range, ramp rates (specifying no-load / loaded conditions), inner chamber dimensions and tolerances, temperature uniformity & fluctuation, communication protocols and data storage formats. For special functions such as nitrogen purge, thermal load adaptation and explosion-proof protection, implementation methods and acceptance criteria must be documented. 5.2 Acceptance Test Items Key on-site acceptance tests: Measured ramp rates under no-load conditions; Ramp rate stability verification under loaded conditions; Multi-point measurement of chamber temperature uniformity; Validation of cyclic test programs; Communication connection and data export verification. Third-party calibration in accordance with JJF 1101-2019 is recommended, with a CNAS-accredited calibration report issued. 5.3 Lead Time & After-sales Support Standard models: 7–15 working days delivery. Non-standard custom chambers: within 20 working days. Operation training and maintenance service are provided after acceptance. The equipment integrates multi-level safety alarms for overtemperature, compressor overload and fan failure to support long-duration continuous thermal cycling tests. VI. Conclusion The core value of non-standard custom thermal cycling chambers lies in the paradigm shift from “adapting tests to equipment” to “tailoring equipment for your tests”. Customised design ensures every equipment parameter precisely matches customer products, test standards and production workflows. Lab Companion TC thermal cycling chambers are built upon standard specifications: -70℃ ~ +150℃ temperature range, 5–25℃/min five-level ramp rates and 34L–16,000L volume coverage. Extended customization covers temperature range, chamber dimensions, ramp rate and dedicated special functions. Backed by Dongguan manufacturing capacity and nationwide service network, we deliver complete reliability test solutions from standard units to bespoke custom chambers for semiconductor, automotive electronics, new energy and aerospace industries. Detailed technical specifications and configurations can be further discussed according to actual test requirements.
    إقرأ المزيد
  • Lab Companion Temperature Cycling Test Chamber for Electronic Components: Selection Guide Focusing on Temperature Uniformity and Anti‑Condensation Design Lab Companion Temperature Cycling Test Chamber for Electronic Components: Selection Guide Focusing on Temperature Uniformity and Anti‑Condensation Design
    Oct 14, 2026
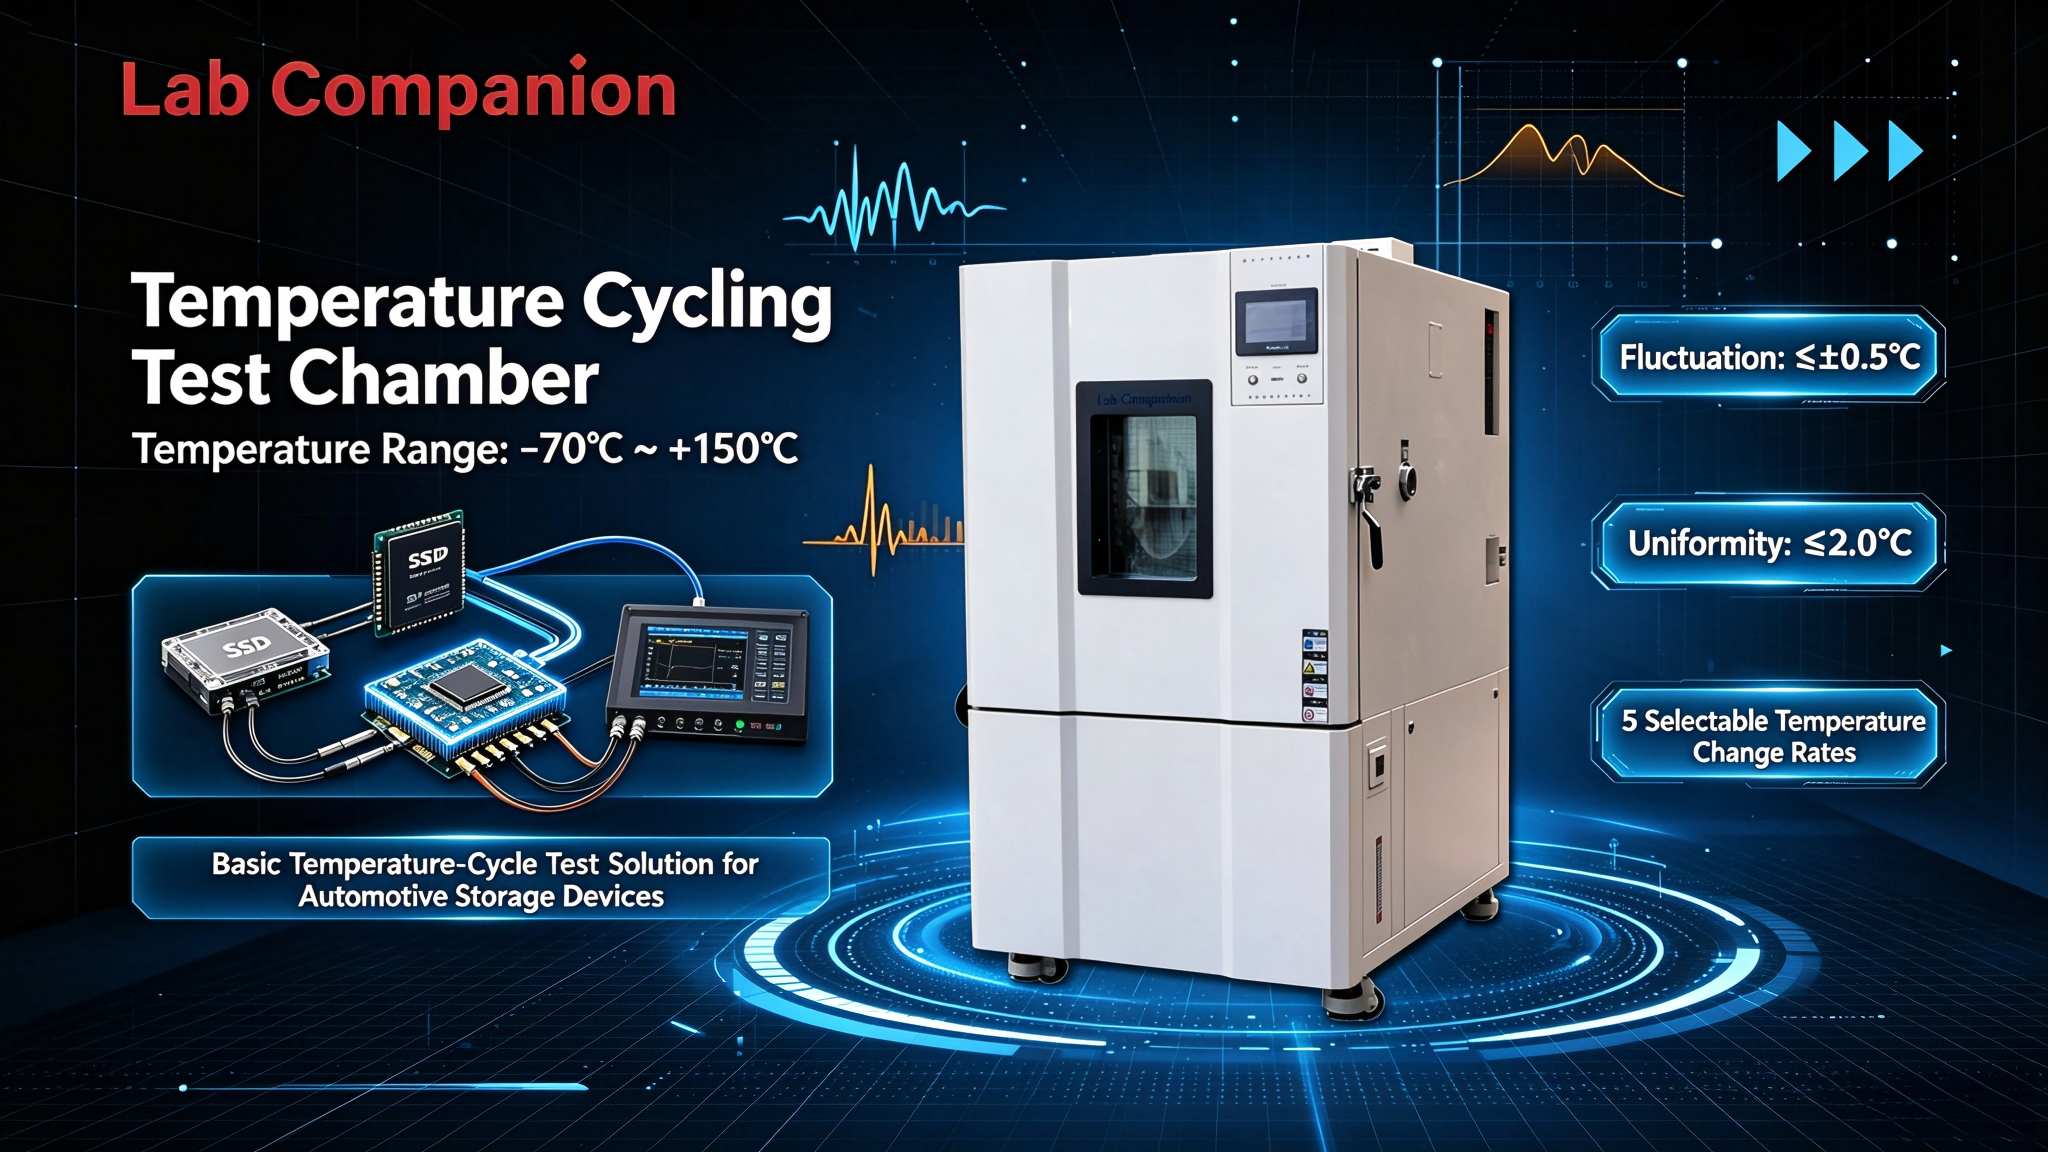
    1. Core Requirements for Temperature Cycling Test of Electronic Components 1.1 Necessity of Component‑Level Reliability Verification Electronic components including capacitors, resistors, connectors, sensors and integrated circuits serve as fundamental building blocks for all electronic devices. During service, these components are subjected to temperature variations. Divergent coefficients of thermal expansion among different materials generate cyclic thermal stress at solder joint interfaces, inside packages and material bonding interfaces under repeated temperature cycling. Long‑term stress may cause solder joint fatigue, package cracking and bond‑wire breakage. Such failures cannot be detected under ambient‑temperature tests and will only emerge under cyclic alternating thermal stress. As a fundamental reliability validation method, temperature cycling test simulates temperature fluctuations during assembly, soldering and field operation, so as to evaluate mechanical and electrical integrity of components under alternating thermal stress. Specified by JEDEC JESD22‑A104, the standard for semiconductor device temperature cycling test, typical test conditions cover the range from ‑65 °C to +150 °C, with dwell time of 10‑15 minutes, temperature transition rate ≥15 °C/min and up to 1000+ test cycles. 1.2 Special Requirements for Test Chambers for Component Testing Characterized by small dimensions, large test batch sizes and dense electrical interfaces, electronic components impose distinct requirements compared with complete‑unit or large‑assembly testing. Temperature Uniformity: Excessive temperature deviation inside the chamber creates inconsistent thermal stress across samples in one batch and increases dispersion of test results. Anti‑Condensation Performance: Condensation forming on component surfaces or pins during temperature ramp‑up from low temperature may lead to short‑circuits and deviation in electrical parameter measurement for powered‑on tests. On‑line Monitoring Compatibility: Dedicated cable ports shall be available to route test harnesses out of the chamber for powered‑on monitoring. Batch‑Loading Capability: Fixture loading efficiency and contact reliability directly determine overall test throughput. 2. Lab Companion Complete Solution for Electronic‑Component Temperature Cycling Test 2.1 Corporate Strength & Manufacturing System Lab Companion (Guangdong Hongzhan Technology Co., Ltd.), founded in 2005 in Dongguan, is a National High‑Tech Enterprise and Guangdong Specialized‑Refined‑Differential‑Innovative Enterprise with over 20‑year experience in environmental reliability test equipment. The company operates under ISO 9001, ISO 14001, ISO 45001 and ISO 27001 management systems, and its products hold CE certification for EU markets. Three manufacturing bases are located in Dongguan, Kunshan and Chongqing. The Dongguan headquarters functions as the R&D center and main production site for standard chambers, covering a plant area of 27 286 m² with an annual output of approximately 1 000 environmental test chambers. 2.2 Key Performance Specifications of Temperature Cycling Chambers Standard temperature range: ‑70 °C ~ +150 °C, expandable up to +180 °C, fully covering temperature requirements defined in JESD22‑A104 and other mainstream semiconductor temperature‑cycling standards. Available temperature ramp rates: 5 °C/min, 10 °C/min, 15 °C/min, 20 °C/min, 25 °C/min. Both linear and non‑linear temperature profiles are supported to meet ramp‑rate requirements of diverse test standards. Temperature fluctuation: ≤±0.5 °C; temperature deviation: ≤±2 °C. 2.3 Temperature Uniformity and Anti‑Condensation Design Adopting dual‑air‑duct circulation together with multi‑point temperature sensor layout, the chamber achieves temperature uniformity ≤±2 °C under full‑load condition and ≤±0.5 °C under steady‑state conditions. This minimizes thermal‑stress discrepancy among components at different positions and suppresses data dispersion for batch testing. The built‑in anti‑condensation system prevents dew formation on component pins and housings during low‑to‑high temperature ramp‑up, ensuring stable powered‑on on‑line testing. The observation window adopts multi‑layer conductive‑film tempered insulating glass with surrounding heating wires to eliminate frosting and fogging at low temperatures for clear visual sample inspection. 2.4 Chamber Volume, Fixture and System Compatibility Standard chamber volumes: 34 L, 64 L, 100 L, 180 L, 340 L, 600 L, 1000 L. Custom non‑standard volumes from 80 L to 8000 L are available. Models can be selected according to component package dimensions and batch sizes, with custom‑designed loading fixtures offered upon request. Extended multi‑channel temperature acquisition enables multi‑point chamber‑field monitoring. Dedicated cable ports are reserved for on‑line electrical‑parameter measurement. The chamber supports connection to host PCs and LIMS laboratory management systems for automatic recording and export of test curves and datasets. 3. Typical Application Scenarios Passive Components (Capacitors & Resistors) Focus validation on capacitance drift, resistance shift and solder‑joint reliability under temperature variation. Compact‑volume chambers suit high‑volume batch testing and comply with industry specifications for passive‑component temperature cycling. Connectors & Sensors Evaluate contact‑resistance variation, material aging and sensor output drift under thermal cycling. Multi‑channel temperature acquisition monitors real‑time thermal conditions around DUTs (Devices Under Test). Integrated Circuits & Semiconductor Devices Temperature range and ramp‑rate options satisfy JESD22‑A104 requirements covering consumer‑grade to automotive‑grade semiconductors, supporting continuous durability testing for up to thousands of cycles. PCB Assembly‑Level Validation Large‑volume chambers accommodate complete PCB assemblies. The programmable controller automatically executes multi‑segment complex temperature profiles for board‑level component reliability assessment. 4. Key Selection Guidelines 4.1 Match Temperature Ramp Rate with Applicable Test Standards Ramp‑rate requirements vary across component specifications. JESD22‑A104 specifies ≥15 °C/min for certain test conditions, while other industrial standards may require 5‑10 °C/min. Select ramp‑rate options strictly per applicable test specifications to avoid over‑specification or insufficient performance. 4.2 Temperature Uniformity for Batch Testing For large‑scale simultaneous testing, temperature uniformity is critical to test‑data credibility. Lab Companion chambers maintain ≤±2 °C uniformity under full‑load. For high‑precision applications, steady‑state performance can be further evaluated. 4.3 Pre‑define Fixture Requirements and Electrical Interfaces Powered‑on on‑line testing is common for electronic components. Define harness quantity and dimensions at the selection stage to confirm proper cable port sizing. Custom fixtures can be developed for specific component packages. 4.4 Balance Chamber Volume Between Throughput and Thermal‑Field Performance Determine required volume based on sample quantity per test run. Insufficient volume reduces throughput; excessively large volume increases difficulty in maintaining homogeneous thermal field. Standard‑volume models are preferred, and non‑custom solutions are applied for special test conditions. 5. Conclusion Three core indicators dominate electronic‑component temperature‑cycling testing: temperature‑field uniformity, anti‑condensation capability and batch‑sample loading performance. Lab Companion temperature cycling chambers deliver wide temperature range of ‑70 °C ~ +150 °C, multi‑step ramp rates from 5 °C/min to 25 °C/min and temperature fluctuation ≤±0.5 °C. Supported by dual‑air‑duct circulation and proven anti‑condensation technology, alongside flexible volume options ranging from 80 L to 8000 L and custom fixture services, our chambers provide complete reliability‑test solutions for semiconductors, passive components and PCB assemblies. Further technical proposals can be customized against your exact test conditions.
    إقرأ المزيد
  • Lab Companion Temperature‑Humidity Cycling Test Chamber: Application of Combined Temperature‑Humidity Environmental Simulation in Electronic Reliability Validation Lab Companion Temperature‑Humidity Cycling Test Chamber: Application of Combined Temperature‑Humidity Environmental Simulation in Electronic Reliability Validation
    Oct 13, 2026
    1. Why Combined Temperature‑Humidity Testing Is Critical for Reliability Validation 1.1 In‑service Products Are Exposed to Coupled Temperature and Humidity Real‑world operating conditions for electronic products never involve temperature stress in isolation. Automotive ECUs in engine compartments undergo drastic temperature swings while being subjected to high humidity from rain and snow. Energy‑storage battery systems may suffer internal condensation inside enclosures due to day‑night temperature fluctuations. Communication base stations deployed in coastal areas operate under prolonged alternating high‑temperature and high‑humidity conditions. Temperature‑humidity coupling triggers multiple failure modes: high humidity accelerates electrochemical corrosion of metal pins; condensation on circuit boards under low‑temperature & high‑humidity conditions may cause short‑circuits; repeated thermal‑humidity cycles lead to aging and cracking of sealing materials. Combined temperature‑humidity cycling test serves as a standardized validation method to replicate such real‑world service conditions. 1.2 Differences Between Coupled Temperature‑Humidity Test and Single‑factor Test Temperature‑only cycling evaluates structural integrity and electrical stability under thermal stress. Humidity‑only testing focuses on material moisture absorption, insulation performance and corrosion susceptibility. Combined testing creates far more complex test conditions. Saturated moisture‑holding capacity of air inside the chamber changes continuously with temperature. At low temperatures, air can hold far less water vapor. Poor control will result in unintended condensation or even frost formation on test samples. For instance, IEC 60068‑2‑30 defines cyclic damp‑heat testing with 12‑hour high‑temperature high‑humidity dwell followed by a 12‑hour cooling phase, intentionally generating condensation on specimen surfaces. This test imposes strict requirements on synchronized temperature‑humidity control of test equipment. 1.3 Industry Standard Requirements for Temperature‑Humidity Cycling In international standards, IEC 60068‑2‑30 specifies the general method for cyclic damp‑heat tests to assess component and equipment performance under combined high‑humidity and temperature‑cycling conditions. IEC 60068‑2‑38 describes combined temperature‑humidity cyclic testing procedures. For automotive electronics, ISO 16750‑4 defines dedicated temperature‑humidity cycling requirements for electronic units mounted at different vehicle locations. Corresponding specifications also apply to photovoltaic modules and energy‑storage systems in the new‑energy sector. 2. Core Technical Challenges of Combined Temperature‑Humidity Test Chambers 2.1 Humidity Tracking Control During Temperature Ramping Compared with pure thermal cycling chambers, the key capability of combined temperature‑humidity chambers lies in synchronous humidity tracking along programmed temperature profiles during rapid temperature changes. Take the cooling process from +85 ℃ / 85 %RH down to ‑40 ℃ as an example: saturated water‑vapor capacity drops sharply as temperature decreases. Without active humidity regulation, relative humidity inside the chamber will surge rapidly and produce unwanted condensation on samples. Excessive dehumidification, on the other hand, drives humidity below setpoints and causes non‑compliant test conditions. The control system must calculate real‑time variation of saturated moisture capacity according to temperature change rate, and dynamically adjust humidification and dehumidification output to keep relative humidity within allowable tolerances. 2.2 Condensation Management and Specimen Protection Certain standards such as IEC 60068‑2‑30 require intentional condensation to evaluate product resistance to damp heat. However, excessive condensation in most other test scenarios may trigger sample short‑circuits and distorted test results and must be properly managed. Equipment shall support configurable condensation‑control strategies, including cooling‑rate limitation, humidity‑setpoint adjustment, pre‑heating and defrost functions. Lab Companion units are equipped with standard anti‑unintended‑condensation logic to avoid unexpected dew formation on specimen surfaces during low‑temperature‑to‑high‑temperature ramps. 2.3 Humidity‑sensor Performance at Low Temperatures Conventional capacitive humidity sensors normally work reliably above 0 ℃. Below 0 ℃, frost buildup on sensor probes causes measurement drift and inaccurate readings. Test chambers shall adopt humidity‑measurement solutions with low‑temperature compensation or indirect calculation via wet‑bulb / dry‑bulb conversion for valid humidity evaluation under sub‑zero conditions. 3. Technical Solution of Lab Companion Temperature‑Humidity Cycling Test Chamber Lab Companion is a national high‑tech enterprise and Guangdong‑province‑level specialized & sophisticated enterprise based in Dongguan, Guangdong, China. 3.1 Temperature‑humidity Range & Thermal‑ramp Performance Temperature range: ‑70 ℃ ~ +150 ℃ Humidity range: 25 %RH ~ 98 %RH (at 20 ℃ ~ 85 ℃); optional low‑humidity version down to 5 %RH Temperature fluctuation: 0.5 ℃; temperature deviation: ±1.5 ℃ Humidity deviation: ±3.0 %RH (>75 %RH); ±5.0 %RH (≤75 %RH) Temperature ramp rate: 5 ℃/min, 10 ℃/min, 15 ℃/min, 20 ℃/min, 25 ℃/min; linear & non‑linear modes supported Effective rapid‑ramp working range: ‑40 ℃ ~ +85 ℃, ‑55 ℃ ~ +125 ℃ 3.2 Temperature‑humidity Conditioning System The chamber adopts balanced temperature‑humidity control. Humidification is realized by steam generation from heated water pan. Dehumidification is achieved via vapor condensation on refrigerated evaporator surfaces. Throughout thermal cycling, the controller dynamically modulates humidification‑dehumidification output based on real‑time ramp rate and humidity deviation to maintain stable humidity tracking against temperature profiles. Product link: https://www.labcompanion.cn/labcompanion_Product_2064188703.html?_v=1708161593 3.3 Chamber Volume & Mechanical Construction Standard volumes: 80 L, 150 L, 225 L, 408 L, 800 L. Standard models are available from stock. Custom volumes from 80 L up to 8000 L are supported. Inner chamber: SUS304 brushed stainless‑steel plate; outer cabinet: cold‑rolled steel with electrostatic powder coating Insulation: rigid polyurethane foam to minimize cold‑loss at low temperature and heat‑loss at high temperature Observation window: multi‑layer hollow electrically‑heated glass to prevent window condensation for clear specimen viewing 3.4 Controller & Data Management A 7‑inch color touch‑screen programmable controller with multi‑language interface supports multi‑segment profile editing. Users can configure ramp rates, humidity setpoints, dwell duration and cycle counts. Test data and curves are recorded automatically. Historical logs can be exported via USB port. Communication interfaces are provided for LIMS integration to enable automatic data upload and report generation. 4. Typical Application Scenarios Automotive Electronics For ECUs, on‑board sensors, infotainment control units and other vehicle‑borne electronics, the chamber performs temperature‑humidity cyclic aging tests complying with ISO 16750‑4, verifying circuit and component reliability under alternating damp‑heat stress. Its wide thermal range covers ‑40 ℃ ~ +125 ℃ for automotive‑grade validation. New‑energy Industry Applied to battery modules, BMS, high‑voltage connectors, on‑board chargers and other e‑powertrain components. Temperature‑humidity cycling evaluates enclosure sealing performance and insulation stability under damp‑heat alternation for new‑energy electronic reliability verification. Industrial Control Suitable for PLCs, frequency converters, industrial power supplies and other complete units to simulate high‑temperature high‑humidity industrial field conditions and validate long‑term operational reliability. Large‑volume TC/TH series accommodates full‑size equipment and supports live‑powered specimen testing. 5. Key Selection Guidelines Match temperature‑humidity specifications: Confirm required temperature and humidity parameters according to product test standards. Narrow‑range models can be selected for high‑temperature‑only high‑humidity testing to control costs. For low‑temperature high‑humidity applications, verify actual humidity‑control performance under sub‑zero conditions. Thermal ramp rate & humidity‑tracking capability: Higher ramp rates impose greater demands on humidity‑following performance. Verify humidity tolerance under target ramp‑rate conditions. For projects requiring both rapid temperature change and precise humidity control, loaded sample validation is recommended during model‑selection phase. Chamber volume & specimen compatibility: Determine chamber size based on sample dimension and quantity. Reserve extra space for wiring and fixtures for live‑powered testing. Data‑interface compatibility: Confirm communication protocol and data format in advance if integration with LIMS or MES systems is required. 6. Conclusion Major technical challenges of combined temperature‑humidity cycling testing lie in reliable humidity tracking during fast temperature transitions and controllable condensation management. Lab Companion temperature‑humidity cycling test chambers deliver a proven solution for automotive‑electronics, new‑energy and industrial‑control customers, featuring wide temperature range of ‑70 ℃ ~ +150 ℃, humidity coverage from 25 %RH to 98 %RH, multiple ramp‑rate options from 5 ℃/min to 25 ℃/min, balanced temperature‑humidity control algorithm, flexible volume customization from 80 L to 8000 L, plus robust local manufacturing and delivery capabilities based in Dongguan, China. Further configuration adjustments can be made according to specific test standards and specimen conditions.
    إقرأ المزيد
  • Lab Companion China‑Manufactured Rapid‑Rate Temperature Change Test Chamber: Wide Temperature Range, Multi‑Rate Options and Core Component Selection Analysis Lab Companion China‑Manufactured Rapid‑Rate Temperature Change Test Chamber: Wide Temperature Range, Multi‑Rate Options and Core Component Selection Analysis
    Oct 12, 2026
    1. Industry Background and Technical Demands for Domestic Rapid‑Rate Temperature Change Test Chambers 1.1 Role of Rapid‑Rate Temperature Change Test Chambers in Manufacturing As core equipment for environmental reliability testing, rapid‑rate temperature change test chambers apply fast‑changing thermal stress to products. This accelerates and exposes early failures caused by defects in electronic components, parts or manufacturing processes, enabling failure elimination in advance. In industries including semiconductors, automotive electronics, new energy, aerospace and 5G communications, temperature cycling testing is an indispensable reliability validation procedure before product release. With rising requirements for products’ thermal‑stress resistance, rapid temperature‑change capability has evolved from an optional feature into a mandatory test requirement. 1.2 Technological Evolution of Domestic Equipment: From Follow‑up to Parallel Development A decade ago, the domestic market for rapid‑rate temperature change test chambers was largely dominated by imported solutions. Early local models generally delivered only 3‑5℃/min temperature‑change rates with non‑linear control. Actual time to reach target temperature far exceeded theoretical values, making it difficult to meet strict requirements for temperature‑change rates and cycle counts defined by standards such as GJB 1032 and IEC 60068. After more than ten years of technology accumulation, domestic rapid‑rate temperature change test chambers have achieved substantial improvements in temperature ramping rate, temperature control accuracy and long‑term operational stability. At equivalent performance levels, domestic equipment costs stand at 50%‑70% of imported units. Local suppliers offer faster supply‑chain response, and replacement lead‑time for core components can be shortened to 3‑5 working days. 2. Key Technical Specifications of Domestic Rapid‑Rate Temperature Change Test Chambers 2.1 Wide Operating Temperature Range Temperature range constitutes the fundamental performance indicator. Current mainstream domestic models cover ‑70℃ to +150℃, delivering a total temperature span of 220℃. For extreme‑condition testing of automotive‑grade chips and aerospace‑specific chips, custom‑built versions with ultra‑wide range of ‑80℃ to +200℃ are available. 2.2 Temperature‑Change Rate and Linear Control Performance Temperature‑change rate is the core metric for evaluating chamber performance. Domestic equipment supports multiple selectable rates: 5℃/min, 10℃/min, 15℃/min, 20℃/min and 25℃/min. Under linear mode, temperature varies constantly over the full ramp‑up and ramp‑down cycle, ensuring thermal stress applied to test samples aligns with standard test assumptions. 2.3 Temperature Control Accuracy and Uniformity Temperature‑control accuracy directly determines test‑data validity. Mature domestic chambers achieve temperature fluctuation ≤±0.5℃, temperature deviation ≤±2℃, and chamber‑wide temperature uniformity ≤±2℃ under full‑load conditions. These performances satisfy requirements from standards including GB/T 2423.22 and IEC 60068‑2‑14. 2.4 Chamber Volume and Customization Capability Chamber volume shall match sample dimensions and test batch size. Standard domestic models range from 80L to 1000L, while large‑size non‑standard customization is supported to cover testing from small‑component specimens to full‑scale complete units. 2.5 Core Components and System Architecture Most systems adopt binary cascade refrigeration, equipped with world‑class compressors together with electronic expansion valves and solenoid valves, enabling stable operation at extreme low temperature of ‑70℃. Locally‑developed intelligent controllers are widely deployed, featuring color touch‑screen HMI, multi‑segment program editing, automatic data acquisition and report generation. 3. Technical Solution for Lab Companion TC‑Series Rapid‑Rate Temperature Change Test Chamber 3.1 Brand & Manufacturing Strength Lab Companion was founded in 2005 in Dongguan, China. As a National High‑Tech Enterprise and Guangdong Provincial Specialized‑Refined‑Innovative Enterprise, we have over 20‑year expertise in environmental reliability test equipment. Our operations comply with ISO9001, ISO14001, ISO45001 and ISO27001 management systems, and products carry CE certification for EU markets. With manufacturing bases in Dongguan headquarters, Kunshan and Chongqing, Lab Companion maintains a nationwide technical‑service network. 3.2 Key Performance Parameters of TC Series Standard temperature range: ‑70℃ ~ +150℃, covering full simulation from extreme cold to high‑temperature working conditions Selectable temperature‑change rates: 5/10/15/20/25℃/min; both linear and non‑linear ramping modes supported Valid rate working range: ‑55℃ ~ +125℃ Temperature fluctuation: ≤±0.5℃; temperature deviation: ±2℃ Optional liquid‑nitrogen‑assisted refrigeration for max ramp rate up to 30℃/min Standard chamber volumes: 180L, 400L, 600L, 800L, 1000L; non‑standard custom sizes available from 80L to 8000L. 3.3 Core System Configuration The refrigeration system applies binary cascade refrigeration with premium‑brand compressors, solenoid valves and flow control valves for stable continuous operation down to ‑70℃. Lab Companion self‑developed cold‑balance energy‑saving control technology reduces energy waste caused by simultaneous heating‑and‑cooling conflict in conventional chambers. Actual energy consumption is reduced by 30%‑60% compared with industry‑average counterparts. The in‑house developed intelligent control platform is fitted with large‑size color touch screen. It supports multi‑segment program editing, automatic data logging and one‑click report generation. Network communication enables remote monitoring and centralized management of multiple test units. 3.4 Compliance with International & Military Standards TC‑Series complies with general environmental‑test specifications IEC 60068‑2‑14 and GB/T 2423.22. It also meets military‑standard requirements of GJB 150A and MIL‑STD‑810H for both gradual temperature cycling and abrupt temperature change tests. Its ramping‑rate performance satisfies the environmental‑stress‑screening requirements specified in GJB 1032‑90. 4. Typical Application Scenarios for TC‑Series Semiconductor Industry: Perform temperature cycling testing per JESD22‑A104 to validate reliability of packaging and solder‑joint interfaces under alternating thermal stress. The chamber supports hundreds to thousands of consecutive test cycles and covers mainstream ‑40℃ ~ +125℃ cycling conditions for automotive‑grade chips. Automotive Electronics: Temperature range and ramping rates fulfill AEC‑Q100 and ISO 16750‑4 temperature‑cycling requirements. Suitable for reliability validation of automotive chips, domain controllers, BMS and other vehicle‑mounted components. New‑Energy Industry: Reproduces extreme high‑low‑temperature conditions for large‑size samples such as battery modules and electronic control units. Sufficient temperature envelope and full‑load ramping rates support limit reliability verification for new‑energy three‑electric systems. Aerospace Industry: Custom‑extended temperature range reaches ‑70℃ ~ +220℃, equipped with self‑developed dual‑PID closed‑loop control. It simulates drastic temperature shifts between sun‑exposed and shadowed aerospace environments to verify structural integrity and functional performance of products under extreme thermal variations. 5. Key Selection Guidelines for Rapid‑Rate Temperature Change Test Chambers 5.1 Match Temperature‑Change Rate Against Applicable Test Standards Prioritize the ramping‑rate requirements defined by target test standards. Requirements differ significantly across specifications: GB/T 2423.22: typical rates at 5℃/min, 10℃/min, 15℃/min JESD22‑A104: certain test conditions require ≥15℃/min AEC‑Q100: temperature‑cycling commonly calls for 10‑15℃/min Select rate grades according to actual test specifications to avoid over‑specification or insufficient performance. 5.2 Evaluate Actual Full‑Load Performance Catalog‑stated ramping rates are divided into no‑load rate and full‑load rate. For samples with thermal mass, full‑load rate represents the real‑world effective performance for testing. All published rates for Lab Companion TC‑Series are measured under full‑load conditions. During selection, provide sample weight and heat‑dissipation data so our engineers can evaluate real‑world ramping performance under loaded conditions. 5.3 Consider Chamber Volume together with Fixtures and Cabling Determine chamber volume based on sample dimensions and loading method. For powered‑on testing with external wiring, reserve extra internal space for cable routing. Lab Companion provides non‑standard customization from 80L‑8000L, with optional test‑port and data‑logging interfaces to satisfy electrical‑test requirements. 5.4 Acceptance and Metrological Calibration Upon equipment delivery, engage a CNAS‑accredited metrology institute to perform calibration in accordance with JJF 1101‑2019 and obtain formal calibration reports. During acceptance, measure temperature overshoot, deviation, fluctuation and uniformity across all rate segments to verify compliance against technical agreements. 6. Conclusion Thanks to years of technical advancement, domestically‑manufactured rapid‑rate temperature change test chambers have become highly competitive in ramping capability, temperature‑control accuracy and system stability. Lab Companion TC‑Series rapid‑rate temperature change test chamber features wide temperature range of ‑70℃ ~ +150℃, multiple full‑load rates from 5℃/min to 25℃/min, temperature fluctuation ≤±0.5℃, binary cascade refrigeration and self‑developed intelligent control system. Supported by manufacturing capacity in Dongguan and customization capability covering 80L‑8000L, Lab Companion delivers complete temperature‑change testing solutions from R&D validation to mass‑production environmental stress screening for semiconductor, automotive‑electronics, new‑energy and aerospace sectors. Detailed specifications and configurations can be further discussed based on your actual test requirements.
    إقرأ المزيد
  • Lab Companion Rapid Thermal Cycling Chamber: Wide-Temperature-Range Reliability Validation for Electronic Components Lab Companion Rapid Thermal Cycling Chamber: Wide-Temperature-Range Reliability Validation for Electronic Components
    Oct 09, 2026
    Rapid thermal cycling test serves as a core method for reliability verification and Environmental Stress Screening (ESS) of electronic components. By executing controlled fast temperature ramping cycles, it amplifies alternating thermal stress generated from thermal expansion and contraction of materials, to expose latent early failures in solder joints, packaging and material interfaces. Lab Companion, a manufacturer based in Dongguan, Guangdong, China, developed the TC Series Rapid Thermal Cycling Chamber targeting testing standards for semiconductors, automotive electronics, and optical modules. Featuring wide temperature range, multi-level temperature ramp rates and stable long-term continuous operation performance, the equipment supports full-process testing requirements from R&D characterization to mass-production stress screening. 1. Definition & Boundary of Rapid Thermal Cycling Chamber 1.1 Difference from Conventional Temperature & Humidity Chamber A standard temperature chamber mainly maintains a steady temperature environment or performs slow temperature cycling, with typical ramp rates between 1.2℃/min and 3℃/min, designed for steady-state environment simulation. A rapid thermal cycling chamber boosts the effective temperature ramp rate to 5℃/min ~ 25℃/min, drastically shortening thermal cycle test duration; tests that originally take several days can be finished within hours. More importantly, higher temperature gradient strengthens thermal stress excitation, efficiently triggering potential early failures of products and meeting accelerated test requirements for ESS screening. 1.2 Difference from Thermal Shock Chamber Thermal shock chambers realize abrupt temperature jump via switching between two independent temperature zones, either by moving samples or switching air paths. In contrast, rapid thermal cycling chambers adopt coordinated control of refrigeration and heating systems within a single test chamber, delivering continuous, programmable smooth temperature ramping. Its temperature profile is a continuous curve instead of step jump. These two types of equipment differ fundamentally in thermal stress mechanism, applicable test standards and sample loading methods, and cannot replace each other. Thermal shock focuses on instant extreme temperature impact; rapid thermal cycling better simulates gradual temperature change under real service conditions of products, suitable for temperature cycling tests specified by AEC-Q100, JESD22-A104 and other standards. 2. Key Technical Parameter Breakdown 2.1 Temperature Range & Ramp Rate The standard TC Series chamber covers -70℃ to +150℃, with a wide temperature span of 220℃, covering most temperature cycling assessment ranges for electronic devices. Five optional ramp rates are available: 5℃/min, 10℃/min, 15℃/min, 20℃/min and 25℃/min, supporting both linear and non-linear temperature profiles: • 5℃/min ~15℃/min: For general thermal cycling and automotive electronic ESS, compliant with AEC-Q100 and ISO 16750-4; • 20℃/min ~25℃/min: For stringent accelerated reliability validation. Valid ramp rate working range: -55℃ ~ +125℃, ensuring stable and accurate rate performance within core test temperature zone. 2.2 Linear & Non-Linear Profile Modes Linear Mode: Maintains constant ramp rate throughout heating/cooling process with fixed-slope temperature-time curve. It precisely replicates standard-defined test profiles to guarantee consistent thermal stress input and test repeatability, widely used for compliance testing. Non-Linear Mode: Enables users to customize multi-segment ramps, dwells and nested cycles to build complex temperature sequences, ideal for customized product validation and failure reproduction tests. Two modes are switchable flexibly to accommodate diverse test conditions. 2.3 Temperature Uniformity & Fluctuation Under fast ramping conditions, temperature consistency inside the chamber directly determines test validity. TC Series features temperature fluctuation ±0.5℃, temperature deviation ±2.0℃, and no-load temperature uniformity ≤2.0℃. Uneven temperature field leads to inconsistent thermal stress across samples. Some defects may fail to be triggered, resulting in unreliable screening conclusions. High-precision Pt100 sensors collect temperature data, paired with dynamic regulation of cooling/heating output and airflow design to balance fast ramping and temperature field stability. 2.4 Chamber Volume & Load-Bearing Capacity Standard chamber sizes: 80L, 150L, 225L, 408L, 800L. Custom sizes from 80L up to 8000L are available, suitable for small components, PCBs, subassemblies and complete products. When selecting equipment, ramp rate under loaded condition is critical. Sample thermal mass and self-heating will consume cooling/heating capacity. During selection, thermal mass and power consumption of DUT should be submitted for evaluation to avoid rate decay and temperature overshoot after loading samples, even if parameters meet specs under no-load condition. 3. TC Series Solution from Lab Companion Lab Companion, located in Dongguan, Guangdong, China, is a National High-Tech Enterprise & Guangdong Provincial Specialized, Refined, Characteristic and Innovative Enterprise. With over 20 years of R&D and manufacturing experience in environmental reliability test equipment, our TC Series rapid thermal cycling chamber is engineered for semiconductors, automotive electronics, optical modules and PCBs, dedicated to thermal cycling tests and mass-production ESS. 3.1 Control System Equipped with self-developed Q8 intelligent controller, 7-inch color touchscreen. Up to 1200 programmable test segments. Pt100 sensors sample at 10 Hz to fully capture temperature sequence even under 25℃/min high-speed ramping. Standard interfaces: RS485 and Ethernet. Optional OPC UA / Modbus TCP for seamless MES integration. Supports scanning to input batch information. PDF reports with pass/fail judgment can be auto-generated once tests complete, ensuring full traceability for laboratory and production-line screening. Multiple safety protections including overtemperature, compressor overload, high/low pressure, fan fault and leakage protection enable long-term uninterrupted cyclic operation. 3.2 Refrigeration Architecture & Energy-Saving Control Adopts binary cascade refrigeration system, equipped with world-class compressors, solenoid valves and expansion valves, paired with eco-friendly refrigerants to guarantee stable continuous operation at ultra-low temperature down to -70℃. Proprietary cold-balance energy-saving control technology reduces energy waste caused by simultaneous heating and cooling in conventional equipment. Power consumption is lowered by 30%~60% compared with industry peers, while extending compressor service life. Every unit undergoes minimum 48-hour continuous cycling burn-in and 9-point temperature calibration before delivery to secure performance. 4. Typical Industry Applications 4.1 Semiconductor Devices Performs chip thermal cycling test per JESD22-A104. Materials including silicon die, molding compound and solder have different coefficients of thermal expansion. Repeated thermal cycles introduce alternating stress to excite latent defects within packaging, solder joints and material interfaces for device reliability assessment. 4.2 Automotive Electronics AEC-Q100 requires thermal cycling covering the full operating temperature range of automotive chips, with typical ramp rate of 10\15℃/min and 500\1000 cycles (up to 2000 cycles for stringent grades). ISO 16750-4 recommends ramp rates from 5℃/min to15℃/min. The 10℃/min and15℃/min preset rates of TC Series perfectly match automotive-grade ESS screening requirements, delivering repeatable reliability data for domain controllers, BMS, automotive sensors and AEC-Q100 chips. 4.3 Optical Modules & PCB Assemblies Validates solder interconnection and material interface durability of communication optical modules and PCB assemblies under alternating thermal stress. Custom chamber sizes and fixture interfaces support batch testing of optical modules in various packages. Complete temperature curve logging facilitates root-cause analysis for failure events. 5. Equipment Selection Guidelines 5.1 Match Test Standards First Clarify mandatory ramp rate requirements defined by target standards: • JESD22-A104: ≥15℃/min for certain test conditions • AEC-Q100 thermal cycling: typical 10~15℃/min • ISO 16750-4: recommended 5~15℃/min Select ramp rate according to standard clauses to avoid insufficient specs or over-spec configuration, optimizing capital investment. 5.2 Evaluate Load Performance Sample mass, thermal capacity and self-heating power directly affect achievable ramp rate. For DUT with large thermal mass, provide sample weight, dimension and heat dissipation parameters at quotation stage to evaluate real ramp rate under loaded condition. Choose standard volume or customized chamber from 80L to 8000L based on sample layout and loading method. 6. Conclusion Rapid thermal cycling chambers are critical assets for electronic component thermal cycling verification and ESS. Lab Companion TC Series, designed and manufactured in Dongguan, China, delivers -70℃ ~ +150℃ wide temperature range, 5~25℃/min adjustable linear ramping and ±0.5℃ temperature fluctuation. Combined with powerful programmable control, MES connectivity and strict factory burn-in, we provide integrated equipment solutions from R&D validation to mass-production screening for semiconductor, automotive electronics and optical communication industries. Custom specifications and configurations can be further discussed based on test standards and DUT conditions.
    إقرأ المزيد
  • Lab Companion|CPO & Optical Engine Thermal Cycling Test Solutions
    Sep 27, 2026
    1. CPO Industry Transition: From Lab Validation to Mass Production Driven by the rapid expansion of AI computing clusters, optical interconnection architectures are accelerating the shift from traditional pluggable optical modules to Co-packaged Optics (CPO) and Near-packaged Optics (NPO). Leading global players are scaling next-generation CPO switching platforms, while Chinese manufacturers are advancing prototype verification and mass production layout, pushing CPO from technical exhibition scenarios toward commercial deployment. By co-packaging optical engines and switch chips on a single substrate, CPO shortens optical signal transmission paths and reduces power loss. However, this highly integrated structure brings higher thermal density and more complex temperature stress distribution. At the mass-production stage, the core industry challenge is no longer technical feasibility, but high-reliability, low-cost, and large-scale manufacturability. 2. New Reliability Challenges Brought by CPO Architecture Innovation The rapid growth of large-scale GPU clusters has completely reshaped data center interconnection requirements. Traditional copper cable interconnection cannot meet the high-bandwidth, low-latency demands of AI clusters. Optical interconnection is now deployed closer to computing chips, extending from cabinet-to-cabinet transmission down to chip packaging level. Unlike conventional pluggable optical modules — which can be replaced individually after failure — CPO integrates optical and electrical chips into one sealed package. Any single device failure may lead to the replacement of the entire system. This fundamental change makes temperature cycling reliability the core indicator of CPO mass production qualification. 3. Three Core Barriers Restricting CPO Commercialization 3.1 Ultra-low insertion loss requirements for optical coupling A qualified CPO system requires optical coupling efficiency above 95% and single-joint insertion loss controlled below 0.5 dB, to maintain overall package loss within 1.8–3 dB. CPO packages multiple heterogeneous materials — including silicon photonic chips, laser chips, ceramic substrates, epoxy resin, and copper interconnects — with a thermal expansion coefficient difference of 2–8 times among materials. Repeated temperature cycling generates periodic thermo-mechanical stress, causing nanometer-level displacement of optical fibers and photonics alignment structures, which directly increases optical loss and deteriorates system performance. 3.2 Severe yield superposition risks CPO presents extreme yield superposition effects. Assuming a 95% individual optical engine assembly yield, a single switch chip integrating 32 optical engines will achieve a system-level yield of only 19%. Complex packaging and high integration significantly raise manufacturing thresholds, leading the industry to predict large-scale CPO commercialization will be delayed until 2028–2029. 3.3 Difficult post-maintenance Pluggable modules support rapid on-site replacement. In contrast, CPO’s highly integrated packaging fixes optical engines and switch chips as a whole. Once the laser or optical engine fails, the entire board needs replacement. The industry is promoting external laser source solutions to reduce maintenance costs, placing vulnerable components at replaceable panel positions. 4. Strict Temperature Cycling Reliability Standards for CPO CPO devices face far more stringent thermal reliability tests than traditional optical modules, mainly reflected in thermal failure mechanisms and optical parameter temperature sensitivity. High thermal density inside CPO packages causes thermal interface material fatigue, pump-out, and dry aging during rapid temperature cycling, continuously increasing thermal resistance. Typical failure modes include solder ball fatigue, gold wire bonding fracture, TEC delamination, substrate warpage, and fiber coupling offset — a unique failure mode of CPO devices. Optical engines are extremely temperature-sensitive. The wavelength drift coefficient of DFB lasers is 0.08–0.1 nm/°C. With mainstream DWDM channel spacing of only 0.8 nm, tiny temperature fluctuations will cause wavelength deviation, crosstalk rise, and increased bit error rate. Therefore, CPO temperature cycling tests must monitor real-time optical parameter stability rather than only structural integrity. Global industrial test standards form a complete certification matrix: • GR-468-CORE: Temperature range -40 °C to +85 °C, linear temperature rate ≥ 10 °C/min, minimum 500 cycles, 10-minute dwell time at extreme temperatures. • High-end 1.6T/ LPO upgrade criteria: Extended range of -55 °C to +125 °C, temperature rate ≥ 15 °C/min. • JEDEC JESD22-A104 & IEC 60068-2-14: Mandatory supplier qualification evaluation standards. 5. Lab Companion Full-level CPO Thermal Validation Solutions (China High-end Manufacturing) Lab Companion is a professional environmental test equipment manufacturer rooted in China, with 20+ years of R&D and manufacturing experience in reliability testing equipment. Supported by three major production bases in Dongguan, Kunshan and Chongqing, covering a plant area of over 6,000 ㎡ and an annual capacity of 1,000 sets of environmental chambers, the brand represents high-precision, cost-effective, and stable Chinese industrial manufacturing capabilities for global optical communication and semiconductor customers. Global Service Note: For overseas clients, Lab Companion provides full-process online technical guidance, remote debugging, program setting, and after-sales support. No on-site door-to-door service is available in overseas regions. Professional online support ensures consistent test accuracy and equipment operation efficiency worldwide. 5.1 Optical Engine & Module-level Solution: TC Series Rapid Temperature Change Chamber The Lab Companion TC series is specially optimized for high-density CPO optical engine screening. • Temperature range: Standard -70 °C ~ +150 °C, extended extreme test range -55 °C ~ +125 °C • Temperature rate: 5/10/15/20/25 °C/min (full loaded actual test rate, linear controllable) • High precision control: Temperature fluctuation ≤ ±0.3 °C, uniformity ≤ ±2.0 °C, fully compliant with GR-468 linearity and consistency requirements • Mass production adaptability: Compact chamber structure with multi-layer sample racks, supporting batch screening of hundreds of optical engines per cycle, matching mass production ESS screening rhythm 5.2 System & Rack-level Solution: Walk-in Rapid Temperature Change Chamber For full CPO switch system and server cabinet verification, Lab Companion provides large-scale walk-in temperature cycling chambers: • Volume range: 1,000L–10,000L • Load capacity: 1,000 kg mechanical load, supporting 50 kW DUT self-heating test • Working conditions: -20 °C ~ +55 °C, temperature rate ≥ 5 °C/min • Application: Full-system loaded temperature cycling test for complete CPO switching platforms 5.3 MES docking & full data traceability All Lab Companion test chambers support real-time recording of temperature curves, rate changes, and dwell data. Equipped with standard Ethernet and RS485 interfaces, and optional OPC UA / Modbus TCP protocols, the equipment can seamlessly connect with factory MES systems to build full-lot, full-process quality traceability, meeting international certification audit requirements. 6. Reliability Determines the Long-term Commercial Value of CPO The global CPO market is transitioning from technical verification to large-scale manufacturing. In the next 3–5 years, the core competition of CPO products will focus on mass-production reliability rather than basic technical implementation. From micro-level optical engine stress screening to full-system cabinet-level thermal verification, Lab Companion (China High-end Manufacture) provides standardized, compliant, and efficient temperature cycling test solutions for global CPO and optical communication clients. With reliable Chinese manufacturing quality and professional overseas online after-sales system, Lab Companion supports global customers throughout the entire R&D verification and mass production screening process. As CPO market penetration grows from 0.5% (2026) to 35% (2030), standardized and high-precision environmental reliability test equipment will remain the core guarantee for product long-term stable operation.
    إقرأ المزيد
  • Lab Companion|From Consumer SSDs to High-Speed Optical Modules: Expanding Boundaries of Environmental Reliability Testing Lab Companion|From Consumer SSDs to High-Speed Optical Modules: Expanding Boundaries of Environmental Reliability Testing
    Sep 24, 2026
    1. Evolving Testing Scenarios: Wider Application Coverage Across High-Tech Industries Environmental reliability testing was once dominated by automotive and industrial applications. Today, the testing landscape has expanded rapidly to serve fast-growing high-tech sectors, including consumer storage, high-speed optical communication, semiconductors, and AI computing hardware. Reliability validation has become a mandatory prerequisite for mass production. Consumer electronics no longer require only basic functionality—they demand stable performance across diverse and harsh climatic conditions. The booming deployment of high-speed optical modules for AI data centers further raises the bar for temperature cycling and environmental durability testing. In this competitive market, product consistency, scenario adaptability, and professional testing capabilities have become core benchmarks for global supplier selection. 2. Consumer SSDs: Strict Temperature Cycling Reliability Requirements Consumer SSDs operate under far more complex thermal conditions than standard room-temperature environments. Heavy-load laptop operation, industrial storage deployment, and cross-region mobile usage continuously expose SSD controllers, flash particles, and power circuits to repeated thermal cycling stress. SSD mass testing features two key challenges:large sample volume and cost-effective validation. Lab Companion rapid temperature change test chambers, equipped with multi-layer sample racks, enable high-volume thermal stress screening with precisely controlled temperature rates and cycle times. The solution effectively eliminates early failures while optimizing testing costs. Beyond basic thermal cycling, SSD testing requires full data integrity monitoring throughout the entire test process. Lab Companion systems support seamless integration with third-party storage monitoring tools, synchronizing temperature curve recording and device status logging. This enables engineers to accurately identify failure root causes—whether from environmental thermal stress or firmware logic issues—and ensures complete, traceable test data for certification and R&D iteration. 3. Optical Modules & Passive Optical Components: Non-Negotiable Thermal Cycling Validation Temperature cycle reliability testing is an essential and standardized procedure for optical communication devices. Laser wavelength accuracy and output optical power are highly sensitive to temperature fluctuations, while fiber coupling structures are prone to thermal deformation. Both active optical modules and passive components such as wavelength division multiplexers and optical isolators must undergo full environmental validation in accordance with international standards including GR-468. High-value optical communication devices prioritize testing accuracy and depth over speed. Lab Companion environmental test chambers reserve abundant external interface resources, supporting multi-channel synchronous temperature acquisition and real-time monitoring of optical power, extinction ratio, and other critical optical parameters. This synchronized testing mechanism builds a complete data chain to support product certification, performance optimization, and mass production quality control. 4. Core Equipment Selection Criteria for Diverse High-Tech Testing As testing scenarios diversify from traditional automotive applications to consumer storage and optical communication, global clients have formed three clear selection principles: Scenario-oriented customization. SSD production requires high-throughput batch screening capacity; optical device testing demands multi-point temperature acquisition and external instrument compatibility; large-scale product validation relies on spacious chamber volume and high-load thermal stability. Professional testing requires scenario-matched equipment rather than generalized models. Certified and verified manufacturing strength. Global buyers prioritize actual loaded performance data, standardized management systems, and stable long-term quality. Lab Companion holds ISO9001, ISO14001, ISO45001, ISO27001 and CE certifications, with full international trademark protection under the Madrid System, delivering globally recognized quality and compliance. Complete data traceability. Advanced electronics and optical industries require standardized test archives and fully traceable experimental data. All Lab Companion equipment supports automatic data recording, intelligent report export, and full-process data retention, meeting strict international audit and certification requirements. In addition, turnkey laboratory procurement has become mainstream. Lab Companion supports integrated delivery of rapid temperature change chambers, temperature & humidity chambers, thermal shock chambers, and walk-in environmental rooms, with unified temperature control logic and standardized data formats for unified laboratory management. 5. Lab Companion: Premium Chinese Manufacturing, Global Standard Test Solutions Rooted in China, serving the world. As a leading high-tech and specialized enterprise based in Dongguan, China, Lab Companion boasts 21 years of professional R&D and manufacturing experience in environmental reliability testing equipment. Benefiting from China’s mature high-end equipment manufacturing industrial chain, we deliver cost-effective, high-precision, and durable testing solutions for global clients across semiconductor, optical communication, consumer electronics, automotive, and research sectors. Our flagship TC series rapid temperature change chambers cover a wide temperature range of -70℃ to +150℃ with customizable specifications. The actual loaded temperature change rate reaches 5–25℃/min, up to 30℃/min with liquid nitrogen assistance. Multiple volume options from 80L to 1000L fully adapt to SSD batch screening and high-precision optical component testing. Extended 24-channel temperature acquisition and external instrument docking capability support professional-grade optical communication reliability verification. Optional alternating humidity modules provide 20%–98% RH adjustable humidity range, fully complying with GR-468 and other international industry standards. Standard anti-condensation design, programmable cycle editing, and full data traceability ensure stable and repeatable test results. Supported by three major manufacturing bases in China (Dongguan, Kunshan, Chongqing) with an annual production capacity of over 2,000 units, Lab Companion delivers stable batch delivery capability for global orders. For overseas clients, we provide professional online technical guidance, remote debugging, and lifelong online after-sales support, ensuring efficient project implementation and stable equipment operation without local on-site service. 6. Professional Reliability Testing Empowers Global Tech Innovation As high-tech industries continue to iterate globally, diversified application scenarios raise higher requirements for environmental reliability verification. Professional, standardized, and scenario-tailored testing is the solid foundation for product stability and global market compliance. Adhering to the rigorous craftsmanship of Chinese high-end equipment manufacturing, Lab Companion focuses on technological innovation and scenario customization. We provide global clients with one-stop, high-reliability environmental testing solutions, supporting R&D iteration, international certification, and high-quality mass production of global technological products.
    إقرأ المزيد
  • From Scale Expansion to Quality Upgrade: 21 Years of Environmental Test Equipment Innovation by Lab Companion in Dongguan, China
    Sep 18, 2026
    1. A Defining Turning Point for China’s Environmental Test Equipment Industry In 2026, China’s environmental test equipment industry enters a pivotal transformation phase. After years of scale-driven growth, the sector is now shifting toward high-quality performance, technological sophistication, and high-end localization. Driven by booming demand across optical modules, semiconductors, and AI computing infrastructure, the industry’s competition logic has fundamentally changed—from simple capacity expansion to comprehensive strength in precision, stability, and system reliability. The domestic Chinese market for environmental test chambers has surpassed ¥18.5 billion in 2026. Localized manufacturing penetration has reached 58.7%, while Chinese brands capture 76.8% of the overall market share. This data proves that Chinese substitution is no longer limited to low-end equipment; it is rapidly penetrating high-precision and mission-critical application fields. As a leading Chinese manufacturer rooted in Dongguan’s advanced manufacturing cluster, Lab Companion answers one core industry question: how Chinese-engineered environmental test equipment is replacing imported solutions through decades of accumulated R&D and manufacturing expertise. 2. Strong Downstream Demand Reshapes Global Testing Standards 2.1 Optical Modules: Test Equipment Becomes a Production-Critical Necessity The global high-speed optical module industry is undergoing massive capacity expansion in 2026. Annual shipments are expected to reach 45 million units for 800G modules and 33 million units for 1.6T modules, with 1.6T demand projected to double in 2027. As optical communication systems advance, testing accuracy requirements have become extremely stringent. DFB lasers inside high-speed optical modules feature a wavelength drift coefficient of only 0.08–0.1 nm/°C. In 100 GHz DWDM systems, minor temperature deviations can cause severe crosstalk and increased bit error rates. Compliant with the GR-468-CORE global standard, production validation requires thermal cycling ranging from -40°C to +85°C with a linear temperature change rate of no less than 10°C/min. Under such strict specifications, reliable environmental test chambers have evolved from optional auxiliary devices into indispensable core production equipment for global optical module manufacturers. 2.2 Semiconductor & AI Computing Growth Drives High-End Testing Upgrades China’s semiconductor industry continues large-scale capacity upgrades. In 2026, domestic wafer fabrication and packaging firms announced expansion projects totaling over ¥45 billion in investment. Advanced semiconductor processes demand stricter temperature stability and cycling accuracy, making environmental test chambers essential for chip design verification, wafer manufacturing, and packaging reliability validation. Meanwhile, global AI computing infrastructure is experiencing explosive growth. China’s AI computing demand surged 417% year-on-year in Q1 2026. Modern AI chips commonly exceed 200W power consumption, making hardware highly sensitive to repeated thermal shocks. Temperature fluctuations can cause packaging delamination, solder joint cracking, and long-term performance degradation. This industry trend creates strong global demand for high-load, fast temperature change test solutions capable of simulating real-world operating stress. 3. Industry Competition Shifts from Scale Growth to Technical Quality 3.1 New Competition Focus: Real-World Stability Over Paper Parameters The industry’s competitive benchmark has undergone a major upgrade since 2022. Four years ago, most manufacturers competed on empty-chamber specifications, prioritizing maximum temperature range and top heating/cooling rates. At that time, Chinese brands held only 35% of the mid-to-high-end market. By 2026, customer evaluation standards have matured significantly. Global buyers now prioritize full-load stability, temperature uniformity, long-duration operational reliability, and energy efficiency rather than theoretical parameters. The mid-to-high-end market penetration of Chinese equipment has risen to 58%, marking a decisive shift from low-cost scale expansion to high-value technological competition. 3.2 Localization Enters the High-End Breakthrough Stage China’s independent equipment manufacturing capability continues to improve. The overall localization rate of environmental test equipment increased from 49.6% in 2024 to 52.7% in 2026. Chinese-made equipment has achieved 35.4% penetration in new energy vehicle testing and 28.6% in aerospace reliability verification. Chinese manufacturers deliver clear global advantages: cost-performance, flexible customization, and efficient technical support. While imported equipment still retains marginal advantages in ultra-high precision and extreme fast thermal cycling, Chinese-manufactured solutions are rapidly closing the technological gap and becoming the preferred alternative for global mass production and reliability validation scenarios. 4. Lab Companion: 21 Years of Premium Manufacturing Rooted in China’s Dongguan Industrial Cluster 4.1 China-Based Production Layout: Three Advanced Manufacturing Bases Founded in 2005, Lab Companion is a professional environmental reliability test equipment manufacturer deeply rooted in Dongguan, Guangdong Province—one of China’s most advanced and comprehensive high-tech manufacturing hubs. Benefiting from Dongguan’s complete industrial supply chain, precise component processing capabilities, and mature electronic manufacturing ecosystem, Lab Companion has grown into a globally competitive Chinese brand over 21 years of focused development. The company operates three major R&D and manufacturing bases in Dongguan, Kunshan, and Chongqing, covering a total factory area of 27,286 m² with an annual production capacity of approximately 2,000 units. The product portfolio includes more than 30 categories: temperature & humidity chambers, rapid thermal cycling chambers, thermal shock chambers, HAST accelerated life testers, and large walk-in environmental laboratories. Lab Companion provides full-level reliability testing solutions from component-level verification to complete machine and cabinet-level validation. 4.2 Independent R&D and Global Standard Certification System As one of China’s earliest environmental test equipment manufacturers certified with CE compliance, Lab Companion holds internationally recognized trademarks registered under the Madrid System, covering the EU, UK, Canada, Southeast Asia, and other global regions. The company maintains strict international management standards, including ISO 9001 Quality Management, ISO 14001 Environmental Management, ISO 45001 Occupational Health & Safety, and ISO 27001 Information Security certifications. With independent intellectual property rights in core temperature control algorithms and refrigeration optimization technologies, Lab Companion was officially recognized as a China “Specialized, Refined, Advanced, and Innovative Enterprise” in 2026, achieving full self-control of core technologies. 4.3 High-Precision Products Tailored for Global High-End Scenarios To meet stringent testing requirements for optical modules and semiconductors, Lab Companion’s rapid temperature change series covers a temperature range of -70°C to +150°C, with five adjustable rate levels from 5°C/min to 25°C/min. All cooling and heating rates are verified under full-load operating conditions, ensuring consistent and reliable real-world performance for global production lines. For high-power AI server and GPU testing scenarios, Lab Companion has developed dedicated high-load thermal cycling equipment supporting up to 50kW continuous heat load, effectively solving thermal fatigue, delamination, and solder failure challenges for high-power computing hardware. The self-developed C100 PID fuzzy logic temperature and humidity control system delivers 28%–38% lower energy consumption than the industry average, enabling high precision, high stability, and energy efficiency for global clients. 5. Global Direct Factory Model & Overseas Remote Technical Support Environmental test equipment features strong non-standard customization characteristics. Traditional multi-layer distribution channels often cause delayed communication, inconsistent technical understanding, and increased procurement costs. Lab Companion adopts a direct factory sales model worldwide, enabling global customers to communicate directly with professional R&D and engineering teams without intermediate dealers. Supported by three intelligent manufacturing bases in China, Lab Companion flexibly allocates production resources to ensure stable lead times even during peak global order seasons. Customers obtain genuine factory-direct pricing, customized technical solutions, and consistent production quality. For global overseas clients, Lab Companion provides professional online remote guidance and full-cycle technical support. Unlike regional domestic on-site services, the global support system delivers fast online troubleshooting, equipment calibration guidance, operational training, and remote system optimization, ensuring stable and continuous equipment operation for overseas production and laboratory facilities. 6. Conclusion: Chinese Manufacturing Moves from Scale Advantage to Technical Leadership China’s environmental test equipment industry is undergoing a historic transformation from quantitative expansion to qualitative upgrading. Fueled by global growth in optical communication, semiconductors, and AI computing, Chinese manufacturers are stepping onto the global stage, competing through core precision, stability, and systematic service capabilities rather than low-cost advantages. With 21 years of manufacturing heritage rooted in China’s Dongguan industrial cluster, three national production bases, full-coverage high-end product lines, and efficient global direct service mechanisms, Lab Companion represents a new generation of Chinese high-end equipment brands. As the global industry shifts from scale competition to quality competition, Lab Companion continues to deliver reliable, cost-effective, and technologically advanced testing solutions, establishing a trusted benchmark for Chinese-manufactured environmental test equipment worldwide.
    إقرأ المزيد
  • Lab Companion High-Low Temperature Test Chamber: Endurance Testing for Long-Term Continuous Operation of High-Power Servers Lab Companion High-Low Temperature Test Chamber: Endurance Testing for Long-Term Continuous Operation of High-Power Servers
    Sep 15, 2026
    1. Demands for Long-Duration Continuous Server Operation Testing 1.1 24/7 Server Operation Demands High Endurance from Test Equipment High-power servers deployed in data centers require stable 24/7 continuous operation. Long-term exposure to ambient temperature fluctuations and gradual heat dissipation degradation leads to cumulative thermal stress, causing component aging, performance drift, and unexpected hardware failures. For AI training servers, continuous full-load tasks can last for days or even weeks, resulting in severe heat accumulation and accelerated component fatigue. Short-term functional verification cannot fully reflect real-world server reliability. Long-duration high-temperature continuous testing is essential to expose latent defects triggered by prolonged thermal stress. In such reliability validation scenarios, the long-term operational stability of the test chamber directly determines the accuracy and credibility of test data. 1.2 Industry Standards for Long-Term High-Temperature Aging Testing High-temperature aging testing is a mandatory reliability procedure for server systems. Servers are placed in a constant high-temperature environment of +40℃ to +55℃ and run full-load stress tests on CPUs, memory, and storage devices. Standard test durations range from 48 to 72 hours, while reliability growth tests can extend to hundreds of hours. GB/T 2423.2-2018 specifies a test temperature range of 40℃ to 85℃ for server motherboard high-temperature testing, with adjustable test durations from 24 hours to hundreds of hours and real-time performance monitoring requirements. GB/T 9813.3-2017 mandates a minimum server MTBF (Mean Time Between Failures) of 10,000 hours, requiring 168 hours of fault-free full-load continuous operation. These industry standards strictly require environmental test equipment to maintain precise and stable temperature output during ultra-long continuous operation. 2. Core Technical Advantages of Lab Companion High-Low Temperature Test Chambers for Long-Duration Operation 2.1 Superior Long-Term Temperature Field Stability Lab Companion high-low temperature test chambers feature a wide temperature range of -70℃ to +150℃, with a temperature fluctuation of 0.5℃ and a temperature deviation of ±2℃. While precise temperature control is easy to achieve in short-term tests, maintaining zero drift during hundreds of hours of continuous operation requires systematic optimized design. Equipped with the C100 PID + fuzzy logic control system, the chamber supports automatic self-checking, linear temperature and humidity calibration, and intelligent automatic shutdown. The balanced temperature and humidity control strategy precisely matches heating and cooling output, effectively reducing frequent compressor startup and shutdown and ensuring long-term operational stability. The standard heating rate is approximately 3℃/min (20℃ to +150℃), and the cooling rate is 1.2℃/min (20℃ to -70℃). The chamber can operate stably for hundreds of hours continuously with consistent temperature distribution across the entire test cavity, ensuring uniform thermal stress for all test samples. 2.2 Long-Life Core Component Design for Continuous Workloads To adapt to ultra-long uninterrupted testing scenarios, Lab Companion adopts high-reliability industrial-grade configurations. Key models are equipped with dual-compressor redundant design (one working, one standby), which automatically switches units in case of single compressor failure to avoid test interruption. Built-in soft start and soft stop protection avoids instantaneous current impact; a 3-minute compressor delay protection mechanism effectively extends component service life. The inner chamber adopts SUS304 stainless steel, and all sealing parts use high and low temperature resistant silicone rubber materials, providing excellent aging resistance for long-cycle testing. 2.3 Strict Factory Endurance Verification All Lab Companion test chambers undergo full-load aging tests before delivery to simulate the harshest on-site working conditions. New product models complete more than 1,000 hours of reliability endurance testing, and all finished products pass 72-hour continuous operation, temperature uniformity, and safety protection verification. Internal test data shows that after simulated 3-year uninterrupted operation tests, the temperature rate attenuation is ≤5% and the temperature accuracy attenuation is ≤0.1℃, far better than the industry average of 15%. The redundant system design increases the MTBF by 2.5 times compared with traditional single-unit equipment under 3,000-hour continuous operation conditions. 3. Practical Testing Solutions for High-Power Server Long-Duration Operation 3.1 Standard High-Temperature Continuous Test Procedures Place the server unit inside the test chamber and raise the temperature to the target value (55℃ or 70℃ typical) at a rate no more than 1℃/min. Start formal timing after the internal temperature field stabilizes. Keep the server running full-load stress programs throughout the test, and continuously monitor CPU/GPU temperature, power consumption, fan speed, and system logs. Lab Companion chambers support scheduled startup and automatic timed shutdown, enabling unattended long-cycle testing and avoiding energy waste and idle operation risks. 3.2 Key Control Factors for Long-Cycle Testing Consistent Temperature Uniformity for Multi-Server Parallel TestingLarge-capacity models (600L/1000L/1500L) support simultaneous testing of multiple server units. With a temperature uniformity within ±2.0℃, the chamber ensures identical thermal stress conditions for all samples during long-duration batch testing. Traceable Test Data RecordsThe system automatically records full-process temperature curves and alarm logs, supporting complete data review and abnormal cause analysis after long-cycle testing, ensuring test authenticity and repeatability. Multi-Layer Hardware Protection Prevents Test InterruptionIndependent over-temperature protectors, mechanical pressure switches, and thermal relays provide hardware-level safety isolation, responding within milliseconds to avoid equipment failure and test data loss during hundred-hour continuous tests. 4. Conclusion Lab Companion high-low temperature test chambers deliver reliable, stable, and repeatable environmental simulation for high-power server high-temperature aging and long-duration reliability verification. With a wide temperature range of -70℃ to +150℃, precise temperature control accuracy, and industry-leading long-term operational stability, the equipment fully meets standard 48–72 hour aging tests and ultra-long reliability growth tests of hundreds or thousands of hours. As a professional environmental test equipment brand, Lab Companion provides global customers with standardized equipment and customized reliability test solutions for server, electronics, and semiconductor industries.
    إقرأ المزيد
  • Lab Companion Rapid Temperature Change Test Chamber: Long-Term Stability Ensures Server Reliability Data Credibility
    Sep 14, 2026
    1. The Overlooked Factor: Long-Term Stability of Test Equipment 1.1 Server Reliability Testing Demands Stable Endurance from Test Chambers High-power servers, especially AI training servers, require continuous 7×24 full-load operation in real scenarios. Large-model training tasks often run for days or weeks continuously. Long-duration thermal accumulation accelerates component aging and gradually introduces performance drift and hidden hardware failures. Therefore, server reliability validation cannot rely solely on short-term functional tests. It requires long-duration high-temperature aging tests to expose potential defects caused by sustained thermal stress. Global mainstream standards define clear testing requirements: • GB/T 2423.2-2018: Server motherboard high-temperature test range from 40℃ to 85℃, with test durations ranging from 24 hours to hundreds of hours. • GB/T 9813.3-2017: Server MTBF must exceed 10,000 hours, requiring 168 hours of continuous full-load aging without failure. These strict standards require environmental test equipment to maintain precise and stable conditions for hundreds of hours. In most procurement evaluations, buyers focus heavily on temperature range, ramp rate, and chamber volume, while easily ignoring long-term precision retention — the most critical factor that determines whether server test data is trustworthy. 1.2 How Equipment Drift Misleads Server Reliability Judgments After long-term cyclic operation, test chambers gradually generate parameter drift due to sensor aging, controller offset, and refrigeration system performance degradation. Subtle deviations in temperature accuracy, uniformity, and ramp rate will not trigger obvious equipment alarms, but they directly invalidate long-duration server test results. In high-power server full-load testing, even a 0.5℃ undetected temperature deviation can mask thermal design weaknesses. Poorly optimized server hardware may pass qualification tests mistakenly, bringing severe reliability risks to mass production and data center long-term operation. 2. Root Causes of Precision Degradation & Lab Companion Hardware Solutions 2.1 Three Core Causes of Long-Term Precision Loss Precision degradation is a cumulative aging effect, mainly derived from three systems: 1) Sensor drift Platinum sensors working repeatedly between -70℃ and +150℃ experience gradual resistance drift. Even minor deviations of 0.1℃–0.2℃ are enough to change the pass/fail judgment of high-precision server and semiconductor reliability tests. 2) Control algorithm offset Traditional fixed PID parameters are calibrated under no-load conditions. After long-term full-load server testing, original control parameters no longer match actual thermal loads, causing temperature overshoot, fluctuation, and unstable ramp speed. 3) Refrigeration and airflow decay Compressor efficiency attenuation, condenser dust accumulation, and fan wear gradually destroy internal temperature uniformity, resulting in inconsistent thermal stress for multi-server parallel testing. 2.2 Lab Companion Redundant Hardware Design for Long-Term Stability Lab Companion TC series rapid temperature change chambers adopt systematic anti-aging and redundant design to avoid long-term precision attenuation, fully adapting to server ultra-long-duration full-load tests. Dual-compressor redundant refrigeration system High-speed and low-temperature models are equipped with dual-compressor backup design (one working, one standby). The system automatically switches in case of single-unit failure, ensuring zero test interruption during hundreds of hours of continuous server aging tests. Dual compressors dynamically adjust load operation to avoid long-term full-load fatigue loss. Comprehensive component protection mechanism Soft start and soft stop systems eliminate instantaneous current impact. A minimum 3-minute compressor delay protection effectively extends service life. Built-in hot gas bypass valves stabilize pressure under variable loads and reduce frequent compressor start-stop fluctuations. Durable chamber and sealing structure Adopting SUS304 stainless steel inner chamber and high and low temperature resistant silicone seals, the equipment maintains stable physical performance after thousands of temperature cycles. The stable technical specifications cover -70℃ to +150℃, with temperature fluctuation ≤0.5℃ and temperature deviation within ±2℃. 3. Full-Lifecycle Stability Assurance: Factory Validation + On-Site Operation 3.1 Strict Factory Aging Validation Every Lab Companion chamber completes full-load aging before delivery to simulate the harshest customer working conditions. • New products pass 1,000+ hours reliability endurance tests • All finished products pass 72-hour continuous stable operation inspection Official test data proves that after simulated 3-year non-stop operation, with anti-fatigue structure and dynamic compensation algorithm: • Temperature ramp rate attenuation ≤5% (industry average: 15%) • Temperature accuracy attenuation ≤0.1℃ • Redundant system MTBF increases 2.5 times compared with traditional single-compressor systems 3.2 Industrial Long-Duration Operation Verification A leading automotive semiconductor packaging enterprise in East China deployed two Lab Companion HZ-ESS-800L rapid temperature change chambers (15℃/min ramp rate) for 7×24 batch cyclic reliability testing. With only 4-hour maintenance every two weeks, the units have achieved more than 5,000 hours of non-stop stable operation by Q1 2025. No unplanned shutdown occurred. Customer on-site logs show compressor current, exhaust pressure, and superheat parameters remain stable without long-term drift, fully proving long-term operational consistency under continuous heavy-load conditions. 3.3 Standardized Maintenance System to Sustain Long-Term Accuracy Lab Companion provides a standardized precision maintenance mechanism for long-term server testing scenarios. Users can perform quarterly sensor calibration with CNAS-certified tools or acquire official on-site calibration services. With standardized maintenance logs and annual professional inspection, the chamber consistently maintains high precision: temperature accuracy ±0.1℃~±0.3℃ and temperature uniformity ≤±0.5℃, fully meeting international reliability test standards. 4. Key Operation Guidelines for High-Power Server Testing To ensure credible and repeatable server long-duration test results, three key principles should be followed: 1) Quarterly sensor calibration Long-hour testing accumulates subtle sensor drift. Regular calibration eliminates system errors and ensures authentic thermal stress conditions. 2) Continuous operation log analysis Monitoring compressor status, pressure data, and temperature curve trends enables early detection of performance degradation and avoids unexpected test termination. 3) Full-load temperature uniformity verification High-power servers generate strong self-heating during full-load operation. Ensure chamber temperature uniformity remains stable under heavy load to guarantee consistent test conditions for single or multiple parallel server units. 5. Conclusion Server reliability testing aims to verify long-term operational stability under extreme and continuous thermal stress. The credibility of test results fundamentally depends on the long-term precision stability of the test chamber. Lab Companion rapid temperature change test chambers eliminate long-term drift, unexpected shutdowns, and data inconsistency through redundant hardware design, strict factory aging validation, and standardized lifecycle maintenance systems. The equipment fully supports conventional 48–72 hour server aging and hundreds-to-thousands of hours high-level reliability growth testing. As a professional environmental test equipment brand with 21 years of R&D and manufacturing experience, Lab Companion provides global customers with stable, repeatable, and traceable environmental test solutions, as well as full-cycle technical support from solution customization to after-sales service.
    إقرأ المزيد
  • Lab Companion Temperature Cycling Chamber: AEC-Q100 Qualification Test Practice for Automotive eMMC / UFS / SSD
    Sep 09, 2026
    1. Practical Requirements of AEC-Q100 Qualification for Automotive Storage 1.1 Market Entry Barriers for Automotive-Grade Storage Driven by vehicle intelligence and connectivity, automotive storage devices are seeing rising adoption. Infotainment systems, instrument clusters, T-BOX units, ADAS domain controllers and autonomous driving domain controllers all rely on eMMC, UFS or automotive SSD for data storage. Unlike consumer storage, automotive storage directly impacts driving safety and user experience, requiring far higher reliability. Tier 1 suppliers and OEMs universally mandate AEC-Q100 reliability qualification for storage components during part selection. Products without this qualification cannot be admitted into automotive supply chains. AEC-Q100 is an IC stress test specification defined by the Automotive Electronics Council. It specifies a full suite of reliability tests for automotive ICs before mass release, including temperature cycling, high-temperature operating life, high temperature humidity bias, ESD and latch-up. Temperature cycling is one of the core tests. It verifies package integrity and solder joint fatigue life under repeated thermal swings. For automotive storage, temperature cycling results determine whether a product can pass AEC-Q100 and be listed in OEM approved vendor lists. 1.2 Position of AEC-Q100 in Storage Component Qualification AEC-Q100 classifies devices into four temperature grades based on operating temperature ranges for different vehicle applications: • Grade 3: 0℃ to +85℃ • Grade 2: -40℃ to +105℃ • Grade 1: -40℃ to +125℃ • Grade 0: -40℃ to +150℃ Grade 3 applies to less demanding in-cabin infotainment systems. Grade 2 covers body control, infotainment and T-BOX, which represent most automotive electronic modules. Grade 1 targets harsh environments near engine bays and ADAS domain controllers. Grade 0 serves the most demanding engine and transmission control units. For automotive storage, Grade 2 and Grade 1 are the mainstream qualification levels. Storage for infotainment and body control typically follows Grade 2. ADAS and autonomous driving storage, mounted close to engine compartments or requiring higher reliability margin, usually requires Grade 1. Temperature cycling is a mandatory AEC-Q100 test. Test conditions vary by grade: Grade 2 uses -40℃ to +105℃; Grade 1 uses -40℃ to +125℃. Both require a minimum of 500 cycles. 2. Comparison of Temperature Cycling Conditions: Grade 1 vs Grade 2 2.1 Grade 2: -40℃ ~ +105℃ Condition Breakdown Grade 2 temperature cycling spans -40℃ to +105℃ with a 145℃ delta. This profile simulates extreme real-world cabin conditions: vehicles parked outdoors in cold northern winters may drop near -40℃; after summer sun exposure, electronics behind dashboards can exceed 100℃. Each cycle consists of four phases: ramp from -40℃ to +105℃ (typically 10℃/min to 15℃/min), dwell at +105℃ for ≥10 minutes to stabilize internal sample temperature, ramp down from +105℃ to -40℃, then dwell at -40℃ for ≥10 minutes. One full cycle takes roughly 40–60 minutes. 500 cycles require continuous chamber operation for 330–500 hours (14–21 days). Samples remain powered during cycling, with real-time monitoring of read/write performance and key parameters. 2.2 Grade 1: -40℃ ~ +125℃ Condition Breakdown Grade 1 uses -40℃ to +125℃, creating a 165℃ temperature delta. Compared with Grade 2, the upper temperature limit rises by 20℃ and the thermal delta increases by 20℃. This profile targets storage mounted near engine bays and ADAS controllers, where component temperatures can exceed 105℃ and reach above 120℃ under heavy vehicle load. Raising the maximum temperature to 125℃ substantially increases stress on storage devices: 1. Larger thermal expansion mismatch across different materials creates stronger thermo-mechanical stress on solder joints and package interfaces, accelerating defect exposure. 2. 125℃ approaches the glass transition and creep range of molding compounds and solders, degrading mechanical properties and raising risks of solder fatigue and package delamination. 3. High temperatures accelerate NAND Flash data retention degradation, imposing stricter reliability requirements on storage media. The cycle sequence matches Grade 1 and Grade 2. However, the wider temperature delta extends ramp times. One Grade 1 cycle lasts 50–70 minutes. Completing 500 cycles requires continuous operation for 420–580 hours (18–24 days). 2.3 Test Differences and Selection Logic The core distinction between Grade 1 and Grade 2 lies in maximum temperature and thermal delta, which affects three areas: thermal stress magnitude, total test duration and chamber requirements. Grade 1 generates higher thermal stress and accelerates latent failure modes. Its total test time is 20–30% longer. The 125℃ plateau demands superior heating performance and temperature stability without overshoot. When defining qualification strategy, select the grade based on end application. Grade 2 is sufficient for infotainment, body control and T-BOX. Grade 1 is recommended for ADAS, autonomous driving controllers, engine-bay adjacent hardware, global markets or applications requiring extra reliability margin. A Grade 1 qualified component is backward compatible with Grade 2 use cases, while Grade 2 parts cannot be deployed in Grade 1 environments. Many manufacturers choose Grade 1 qualification upfront to broaden market coverage. 3. Full Workflow of Temperature Cycling Test 3.1 Pre-test: Sample Preparation and Initial Characterization AEC-Q100 temperature cycling includes three phases: pre-test preparation, test execution and post-test evaluation. Pre-test work ensures consistent sample condition and complete baseline data. A minimum of 77 units are randomly sampled from one batch (exact quantity depends on test plan and acceptance criteria). All samples undergo visual inspection to rule out physical damage, package defects or marking issues. Initial electrical characterization is then performed and recorded: functional tests (read/write, erase, bad block management), performance tests (sequential read/write speed, random IOPS), and health checks including SMART attributes, bad block count, wear leveling and initial error rates. Baseline data serves as reference for post-test comparison. Any meaningful parameter shift must be documented and analyzed. Only samples passing initial inspection are loaded into the chamber. Sample loading rules: distribute samples evenly across shelves to avoid localized thermal accumulation. Mount each unit on sockets or burn-in boards connected to external test hosts for live power monitoring. Maintain sufficient air gaps between samples to prevent airflow blockage and temperature non-uniformity. 3.2 Test Execution: Program Setup, Live Monitoring and Cycle Counting During execution, the chamber controller runs a programmed thermal profile: start temperature, ramp rate, high dwell setpoint and duration, low dwell setpoint and duration, plus target cycle count. Grade 2 is programmed for -40℃ / +105℃; Grade 1 for -40℃ / +125℃. Ramp rates are set between 10℃/min and 15℃/min, with minimum 10-minute dwells at extremes and 500 total cycles. Once started, the chamber runs automatically and continuously logs thermal profiles. External test hosts maintain power to DUTs and collect data every 5–10 minutes. Monitored items include power status, read/write integrity, disk dropouts, communication interruptions and abnormal error growth. Critical events such as DUT dropout are timestamped with cycle number. Cycle counting adopts dual control: automatic chamber logging plus daily manual cross-check against temperature curves to confirm validity. If tests stop due to power loss, chamber fault or temperature alarm, engineers review logs and thermal history to decide whether partial cycles count toward the total. AEC-Q100 defines clear rules for interrupted tests; all decisions must follow the standard. 3.3 Post-test: Final Characterization, Failure Analysis and Report Generation After finishing 500 cycles, samples are removed and stabilized for ≥2 hours under standard ambient conditions (15℃–35℃, 25–75% RH) before final testing. Final tests repeat the full initial inspection suite: visual check, functional, performance and health assessment. Acceptance criteria: no visible cracking, deformation or package damage; all read/write functions remain operational without dropouts or communication failures; performance degradation stays within product specification limits; bad block and error count increases remain within acceptable thresholds. Any failed unit triggers failure investigation. AEC-Q100 uses LTPD sampling to determine batch pass/fail based on failure tally. Failed samples go through failure analysis: SAM scanning for package delamination, X-ray inspection for solder cracking, cross-sectioning to observe crack morphology, and electrical fault isolation. FA findings feed design and process improvements. The final test report contains standard reference, test profile, chamber ID/calibration status, sample batch/serial numbers, baseline data, continuous temperature logs, cycle records, real-time monitoring logs, post-test results and failure analysis conclusions. Reports require sign-off by test and review engineers as supporting documentation for AEC-Q100 certification. 4. AEC-Q100 Compliance Capabilities of Lab Companion Temperature Cycling Chambers 4.1 Temperature Range and Accuracy Compliance Lab Companion temperature cycling chambers cover -70℃ ~ +150℃, fully satisfying AEC-Q100 Grade 2 (-40℃ to +105℃) and Grade 1 (-40℃ to +125℃) requirements with ample safety margin. The system maintains stable long-run operation at 125℃ without thermal drift. Performance specifications: temperature fluctuation ≤ ±0.5℃, temperature uniformity ≤2.0℃, temperature deviation ±2.0℃, exceeding GB/T 5170 requirements. AEC-Q100 requires consistent thermal stress across all DUTs. Lab Companion’s ≤2.0℃ uniformity ensures all automotive storage samples experience equivalent thermal loading over 500 cycles, delivering statistically valid test results. Linear ramp rates are configurable from 5℃/min to 25℃/min to precisely replicate AEC-Q100 thermal profiles. 4.2 Long-duration Stability and Data Traceability AEC-Q100 temperature cycling demands uninterrupted operation for 14–24 days. Lab Companion chambers use premium brand compressors and refrigeration components with multi-layer protection: over-temperature, compressor overload and phase-loss protection. Every unit undergoes a minimum 48-hour continuous run-in test before shipment to validate refrigeration and control reliability. Traceability is mandatory for AEC-Q100 audits. The touch controller automatically records temperature curves, cycle counters, alarms and runtime logs. Data can be exported via USB as CSV or PDF files for report archiving. Complete thermal logs serve as objective evidence during certification audits and meet traceability requirements. 4.3 Calibration at Dongguan Factory & Global Service Support Each chamber is assembled and calibrated at the Dongguan manufacturing site. Factory validation includes ramp rate verification, 9-point temperature mapping, extreme setpoint stability testing and continuous runtime validation. For automotive storage customers, pre-run validation for Grade 1 or Grade 2 profiles can be performed to confirm performance under your target test conditions. Delivery includes calibration certificates and validation reports, ready for lab system audits and AEC-Q100 on-site reviews. Our global service network delivers installation, commissioning, periodic calibration and on-site repair. Automotive qualification schedules are tight; rapid service response minimizes downtime caused by equipment faults. Annual maintenance is recommended, including refrigeration inspection, electrical tightening, thermal field recalibration and consumable replacement to sustain accuracy for years of AEC-Q100 testing. 5. Common Issues in AEC-Q100 Qualification and Mitigation 5.1 Test Interruption and Cycle Recounting Power outages, equipment faults or temperature alarms may halt cycling. AEC-Q100 interruption rules: if the stop occurs during temperature dwell, lasts ≤30 minutes and sample temperature remains close to setpoint, completed cycles remain valid. If interruption happens during ramp-up/ramp-down, or temperature deviates significantly, the incomplete cycle is discarded and valid counts must be re-evaluated against thermal logs. Mitigation: deploy UPS backup for power resilience; implement scheduled preventive maintenance; review temperature profiles and chamber status daily; preserve full logs after any outage and consult certification bodies when judging cycle validity. 5.2 Temperature Non-uniformity and Sample-to-sample Variation Poor airflow from overloading, accumulated dust or expired calibration creates uneven thermal distribution. Symptoms include large failure-rate variance across positions in one chamber and inconsistent results across batches. Mitigation: follow sample loading guidelines and preserve airflow channels; regularly clean condensers and air ducts; perform 9-point thermal mapping every 6–12 months to maintain ≤2.0℃ uniformity; mark poor-uniformity zones and avoid placing critical qualification samples there; arrange on-site service for airflow tuning and recalibration when needed. 5.3 Non-compliant Test Reports Auditors frequently reject incomplete reports due to missing ramp rates/dwell times, discontinuous temperature logs, unclear sample serial number traceability, superficial failure analysis or incomplete approval signatures. Mitigation: adopt standardized AEC-Q100 report templates covering all mandatory fields; export native chamber logs to avoid manual transcription errors; maintain sample traceability linking serial numbers, baseline data, runtime logs and post-test results; document full failure analysis for all rejected units; enforce three-level sign-off (test engineer, reviewer, approver). 6. Conclusion AEC-Q100 temperature cycling is a gatekeeper for automotive eMMC, UFS and SSD entering OEM supply chains. The difference between Grade 2 and Grade 1 defines thermal stress intensity, test duration and chamber requirements. Rigorous control across the full test lifecycle — sample preparation, in-test monitoring, post-test characterization and reporting — directly determines qualification success. Lab Companion temperature cycling chambers deliver wide temperature range, precise thermal control, reliable long-run operation and full data traceability, fully supporting AEC-Q100 Grade 1 and Grade 2 qualification for automotive storage. Backed by factory calibration in Dongguan and worldwide after-sales support, Lab Companion provides end-to-end solutions: chamber selection, profile setup and test execution support. We help storage manufacturers complete AEC-Q100 qualification smoothly and gain access to automotive supply chains.
    إقرأ المزيد
1 2 3 4 5 6 7 8
ما مجموعه 8الصفحات

اترك رسالة

اترك رسالة
إذا كنت مهتما بمنتجاتنا وتريد معرفة المزيد من التفاصيل ، فالرجاء ترك رسالة هنا ، وسوف نقوم بالرد عليك في أقرب وقت ممكن.
إرسال

وطن

منتجات

واتس اب

اتصل بنا